
From Assembly to Verification: How DFT Is Changing the Way Modern PCBA Is Designed for Testing
A PCBA That Works Is Not Always a PCBA That Is Easy to Test
A PCB can be electrically correct, mechanically reliable, and successfully assembled—and still create a major problem on the production line.
The problem may appear when engineers try to test it.
Where should the test fixture make contact?
How can hidden faults inside a dense PCBA be identified?
Can the production line distinguish a component failure from a soldering defect?
How quickly can thousands of PCBAs be tested without relying on manual inspection?
These questions lead to a critical but often underestimated concept in electronics manufacturing:
Design for Testability, or DFT.
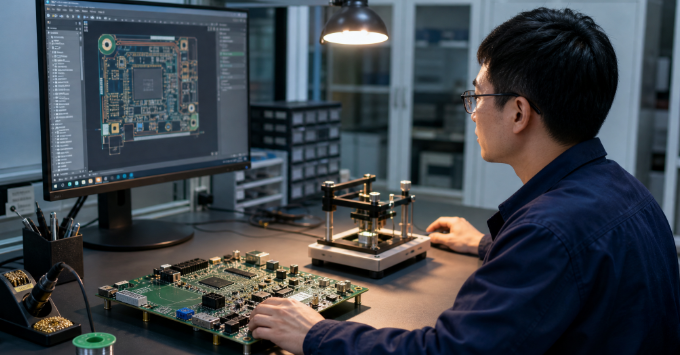
DFT is the practice of designing a PCB and PCBA so that the finished assembly can be tested efficiently, accurately, and consistently.
Instead of waiting until production to determine how a PCBA will be tested, DFT introduces test requirements into the design process itself.
The result is a different approach to PCB development:
Design → Assemble → Test
becomes
Design for Assembly + Design for Test → Assemble → Verify
For modern electronics manufacturers, this shift can significantly improve production efficiency, fault diagnosis, and product quality.
 1. What Is DFT in PCB and PCBA Manufacturing?
DFT stands for Design for Testability.
Its core objective is to make a PCBA easier to verify after manufacturing.
A DFT strategy may consider:
- Test point placement
- Circuit accessibility
- ICT requirements
- Functional testing
- Boundary Scan
- Programming interfaces
- Measurement points
- Test fixture design
- Fault isolation
The concept is straightforward:
If engineers cannot easily access and measure a circuit, testing becomes more difficult.
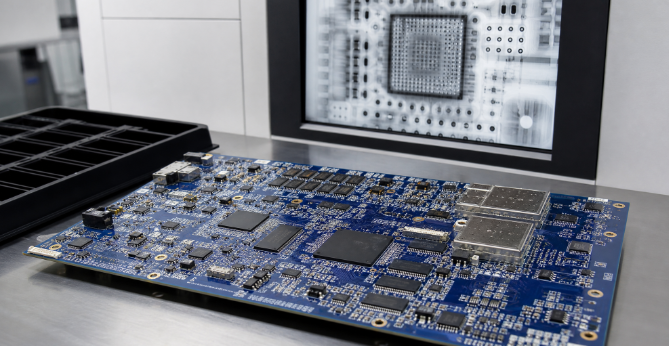
This is particularly important for modern PCBAs containing high component density, multiple PCB layers, BGA packages, microcontrollers, wireless modules, and complex power systems.
2. Why Testing Becomes Difficult as PCBAs Become More Complex
Early electronic products often used relatively simple circuits.
A technician could use a multimeter or oscilloscope to locate obvious problems.
Modern PCBAs are very different.
A single board may contain:
- Microcontrollers
- DDR memory
- Power management circuits
- High-speed interfaces
- RF modules
- Sensors
- Motor drivers
- Multiple voltage rails
Many of these signals are not physically accessible after assembly.
BGA devices are a good example.
Because solder joints are located underneath the package, traditional visual inspection cannot directly verify every connection.
This means manufacturers need a combination of inspection and electrical test technologies.
DFT helps prepare the PCB for these technologies before the first board reaches the production line.
 3. Test Points Are the Gateway to PCBA Testing
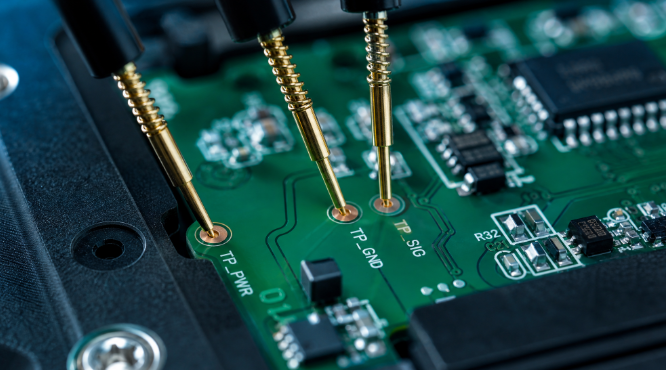
One of the simplest but most important DFT considerations is the test point.
A test point provides an accessible electrical connection that allows automated equipment or test probes to measure a specific circuit node.
Typical test points may be connected to:
- Power rails
- Ground
- Communication signals
- Analog signals
- Digital interfaces
- Critical IC pins
A well-designed test point structure allows engineers to quickly measure important circuit parameters.
However, test points require space.
On highly compact PCBAs, adding dozens of test points can compete directly with component placement and routing requirements.
This creates an engineering trade-off:
Higher Test Coverage vs. Limited PCB Real Estate
The solution is not simply adding as many test points as possible.
The objective is to identify the most valuable electrical nodes.
4. ICT: Testing the PCBA Before It Becomes a Product
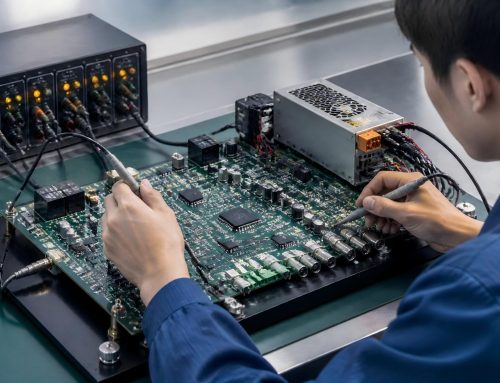
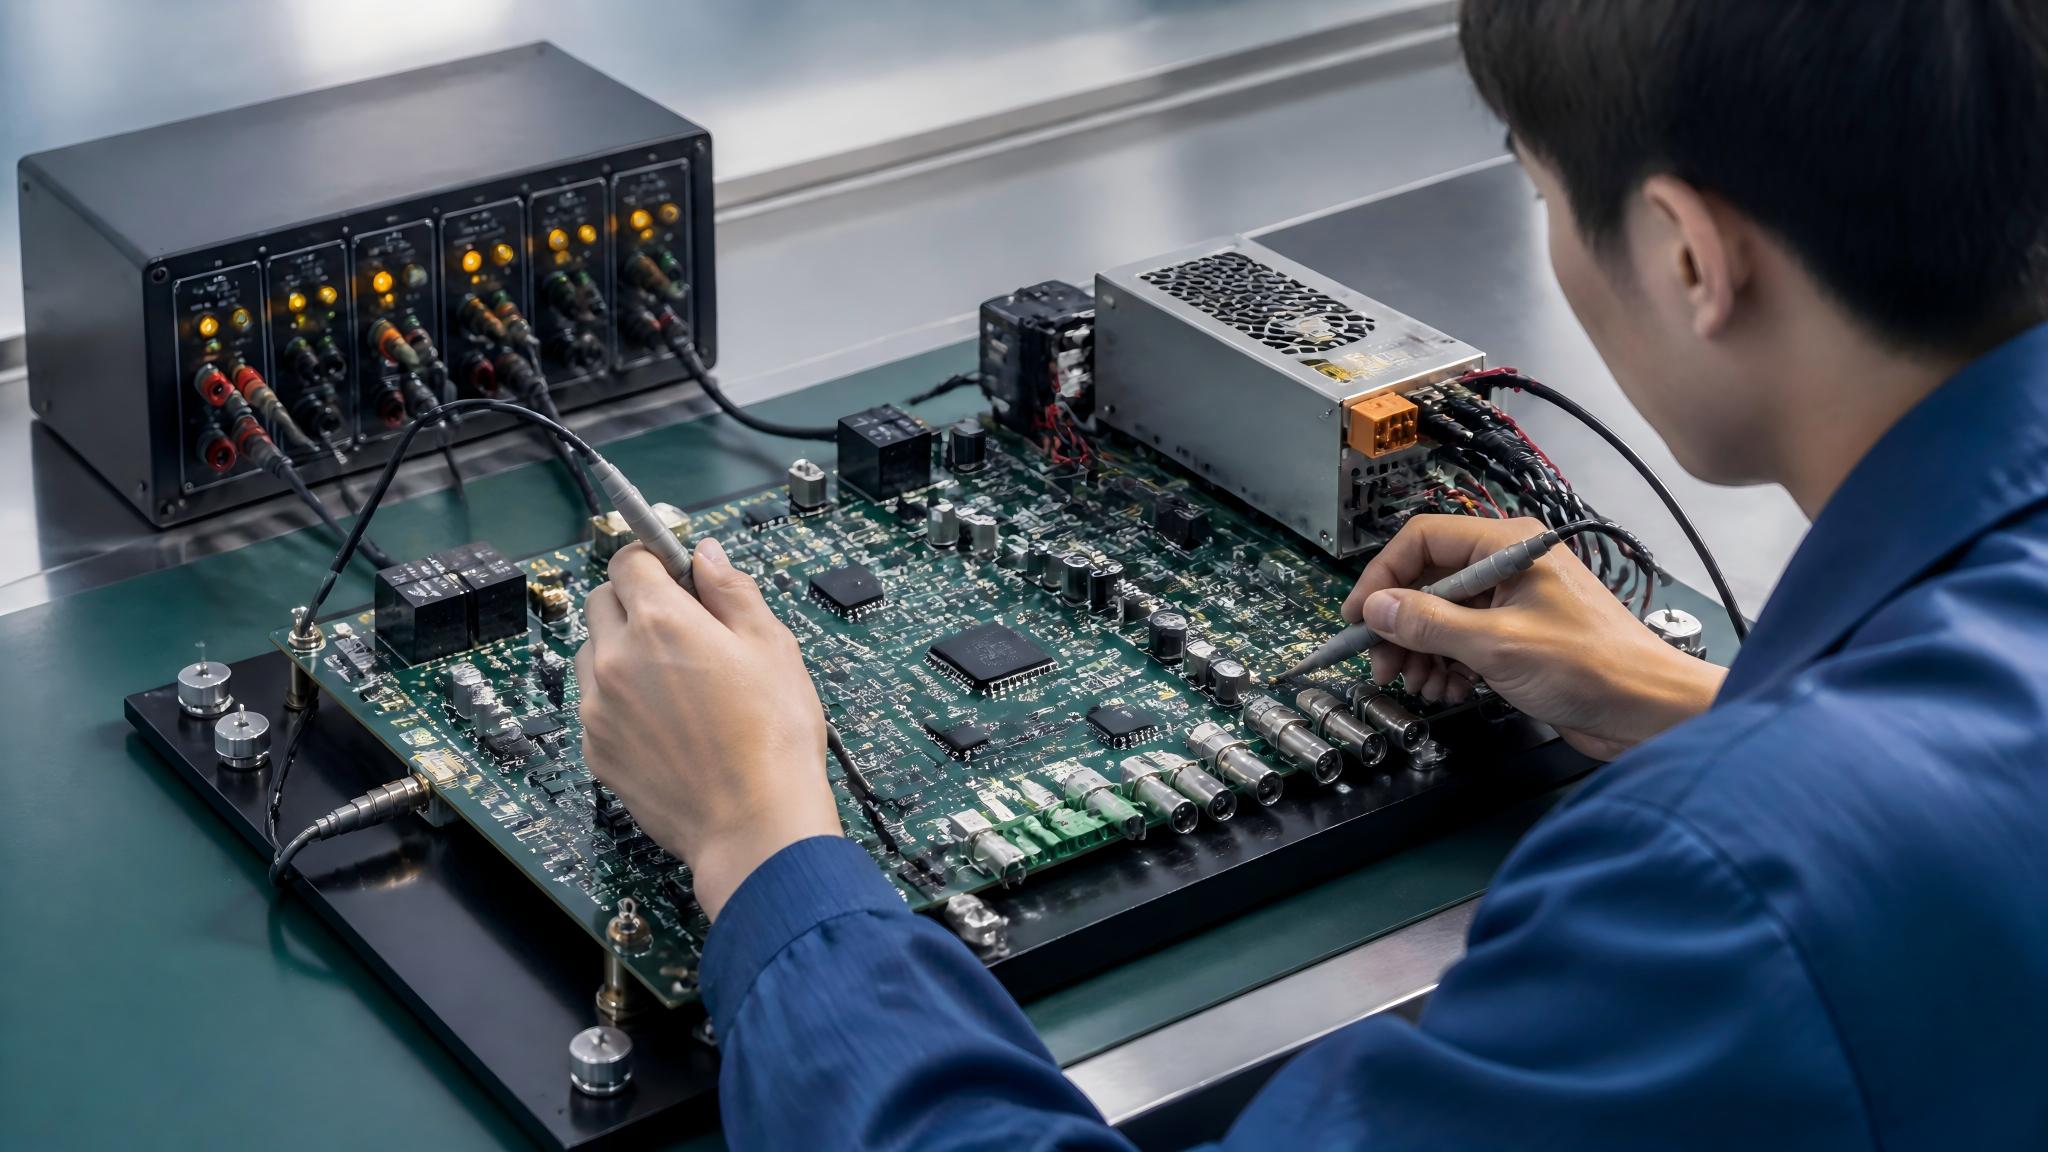
In-Circuit Test (ICT) is widely used for manufacturing verification.
ICT can evaluate individual circuit characteristics by accessing predefined test points.
Depending on the design and equipment, ICT may detect issues such as:
- Open circuits
- Short circuits
- Incorrect component values
- Missing components
- Incorrect component orientation
- Certain component-level electrical faults
The major advantage of ICT is speed and repeatability.
Instead of manually checking individual components, an automated fixture can perform a large number of measurements.
However, ICT performance depends heavily on PCB design.
If critical nodes cannot be accessed, test coverage may be limited.
This is why ICT requirements should be considered during PCB layout rather than after PCB fabrication.
 5. FCT Answers a Different Question: Does the PCBA Actually Work?
ICT mainly focuses on electrical characteristics at the circuit level.
Functional Circuit Test (FCT) approaches the problem differently.
Its central question is:
Does the assembled PCBA perform its intended function?
An FCT system may simulate the real operating environment of the board.
Depending on the product, testing may include:
- Power-up sequence
- Communication interfaces
- Sensor inputs
- Motor outputs
- Display functions
- Audio signals
- Network communication
- Current consumption
- Firmware operation
For example, a controller board may need to communicate with an external device through CAN, UART, USB, Ethernet, or another interface.
An FCT system can verify whether that communication actually works.
6. ICT and FCT Are Complementary, Not Competitive
It is a mistake to assume that one test method can replace every other method.
ICT and FCT answer different questions.
ICT
Focuses on:
“Is the circuit electrically assembled correctly?”
FCT
Focuses on:
“Does the completed PCBA perform its intended function?”
A mature PCBA manufacturing strategy may therefore combine:
SPI → AOI → X-Ray → ICT → Programming → FCT
Each stage catches different categories of problems.
This layered approach can significantly improve defect detection.
7. Boundary Scan Helps Test Highly Dense PCBAs
As PCBAs become denser, physical test access becomes more difficult.
This is where Boundary Scan technology becomes valuable.
Boundary Scan is associated with IEEE 1149.1 and JTAG-based testing.
Instead of relying entirely on physical probes, compatible integrated circuits can provide internal test access through dedicated test structures.
This can help engineers test connections that are difficult to reach physically.
Boundary Scan can be particularly useful for PCBAs containing:
- FPGAs
- Processors
- Complex digital ICs
- High-density interconnects
It provides another pathway for testing complex digital circuits when traditional probe access is limited.
8. Programming Should Also Be Part of the Test Strategy
Modern PCBAs often require firmware before they can perform their intended functions.
That means programming is not simply a software task.
It can become part of the PCBA production process.
Typical production operations may include:
- Board assembly
- Electrical verification
- Firmware programming
- Functional initialization
- Final functional test
The production system may need to record:
- Firmware version
- Programming status
- Serial number
- Programming timestamp
- Test result
This creates a direct connection between hardware and software traceability.
9. Serial Numbers Make Test Results More Valuable
Imagine a production line manufacturing 10,000 PCBAs.
If the factory only records that “the production batch passed testing,” the information is limited.
If every PCBA receives a unique identifier, the situation changes.
A serial number can be connected to:
- PCB lot
- Component information
- SMT production data
- AOI results
- ICT results
- Firmware version
- FCT results
Now engineers can answer a much more precise question:
“What happened to this specific PCBA?”
This is particularly useful for products with long service lifecycles or strict quality requirements.
10. DFT Can Improve Fault Isolation
Testing is not only about determining whether a board passes or fails.
A good test strategy should also help identify why it failed.
Consider a PCBA that does not start.
Possible causes may include:
- Incorrect power supply
- Short circuit
- Failed regulator
- Incorrect firmware
- MCU soldering issue
- Clock failure
- Communication problem
Without appropriate test access, engineers may spend significant time investigating the entire board.
With strategically selected test points, engineers can measure power rails and critical signals step by step.
The failure location can then be narrowed down much faster.
This is one of the hidden benefits of DFT:
Good testability reduces troubleshooting time.
11. DFT Must Work Together With DFM
DFT and DFM are closely related but serve different purposes.
DFM — Design for Manufacturability
asks:
Can the PCB be manufactured and assembled efficiently?
DFT — Design for Testability
asks:
Can the finished PCBA be tested and diagnosed efficiently?
A PCB may be highly manufacturable but difficult to test.
For example, a compact board may provide excellent SMT placement efficiency but leave almost no room for test points.
Conversely, a board may have excellent test accessibility but unnecessarily complicated assembly requirements.
The best PCB design balances both.
DFM + DFT = Production-Ready PCBA
12. DFT Also Influences PCB Layout
DFT should be considered while routing the PCB.
Engineers may need to reserve areas for:
- Test probes
- Fixture access
- Test points
- Programming connectors
- Ground references
Test points should also be positioned so that probes can physically reach them.
This sounds simple, but mechanical constraints can become complicated on high-density PCBAs.
Components, heat sinks, connectors, shields, and enclosures can all obstruct test access.
Therefore, PCB layout should consider both electrical connectivity and physical test accessibility.
13. Test Fixture Design Can Affect Production Economics
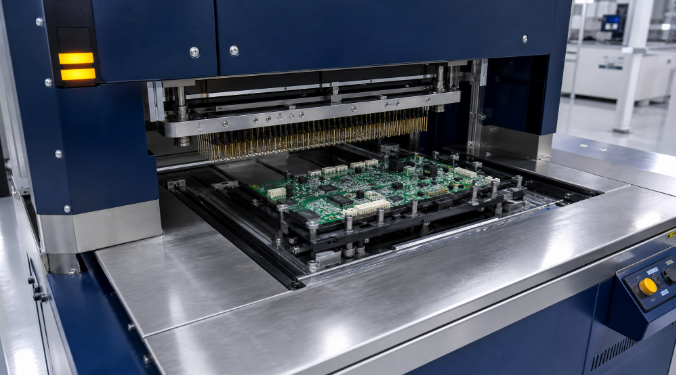
For medium- and high-volume PCBA production, test fixtures can become an important part of manufacturing cost.
A fixture may need to provide:
- Mechanical positioning
- Probe contact
- Electrical connections
- Pneumatic or mechanical clamping
- Interface with automated test equipment
If the PCB layout is not designed with fixture access in mind, fixture development may become unnecessarily complicated.
A well-planned DFT strategy can simplify fixture design.
This can reduce:
- Fixture development time
- Manufacturing cost
- Test cycle time
- Maintenance complexity
Therefore, DFT should be evaluated not only from an engineering perspective but also from a production economics perspective.
14. How DFT Supports High-Volume PCBA Manufacturing
When production volume increases, test efficiency becomes increasingly important.
Suppose a factory produces tens of thousands of PCBAs.
A manual test process may create:
- Long cycle times
- Operator dependency
- Inconsistent results
- Higher labor costs
Automated testing can provide:
- Repeatable procedures
- Faster cycle times
- Automatic pass/fail decisions
- Digital test records
This makes DFT especially valuable when a product moves from prototype manufacturing into mass production.
The test strategy should scale together with the production volume.
 15. DFT Should Begin Before the First Prototype
One of the most expensive mistakes is waiting until prototype assembly is complete before deciding how the PCBA will be tested.
A better development process introduces DFT during the design stage.
A practical workflow can be:
Product Requirements
↓
Circuit Design
↓
Component Selection
↓
PCB Layout
↓
DFM + DFT Review
↓
Prototype PCBA
↓
Test Fixture Development
↓
ICT / FCT Validation
↓
Pilot Production
↓
Mass Production
This approach reduces the possibility of discovering major test limitations after the PCB has already been manufactured.
16. The Future of PCBA Testing Is Moving Toward Intelligent Verification
The future of PCBA testing will not rely on a single machine.
Instead, multiple data sources will increasingly work together.
Production systems may combine:
- SPI data
- AOI data
- X-Ray results
- ICT measurements
- Firmware records
- FCT results
- Serial-number traceability
This creates a complete quality data chain.
When a failure occurs, engineers can compare inspection and test information across different manufacturing stages.
Over time, this data can also support:
- Statistical process control
- Defect trend analysis
- Predictive maintenance
- Automated fault classification
- Process optimization
Testing is therefore evolving from a simple pass/fail gate into an intelligent source of manufacturing information.
The Best PCBA Is Designed to Prove That It Works
In electronics manufacturing, assembling a PCBA is only half of the challenge.
The other half is proving that the finished board has been assembled correctly and performs as intended.
That is why Design for Testability is becoming increasingly important.
A well-designed DFT strategy considers:
- Test points
- ICT
- FCT
- Boundary Scan
- Programming
- Fixture accessibility
- Serial-number traceability
- Fault isolation
from the earliest stages of PCB development.
The key idea is simple:
Do not wait until the PCBA is built to ask how it will be tested. Design the PCB so that testing is part of the product from the beginning.
As PCBAs become smaller, denser, faster, and more intelligent, testability will become an increasingly important part of product design.
The future of PCBA manufacturing is not simply about building boards faster.
It is about building boards that can prove their quality faster, diagnose failures smarter, and enter mass production with greater confidence.
Leave A Comment