
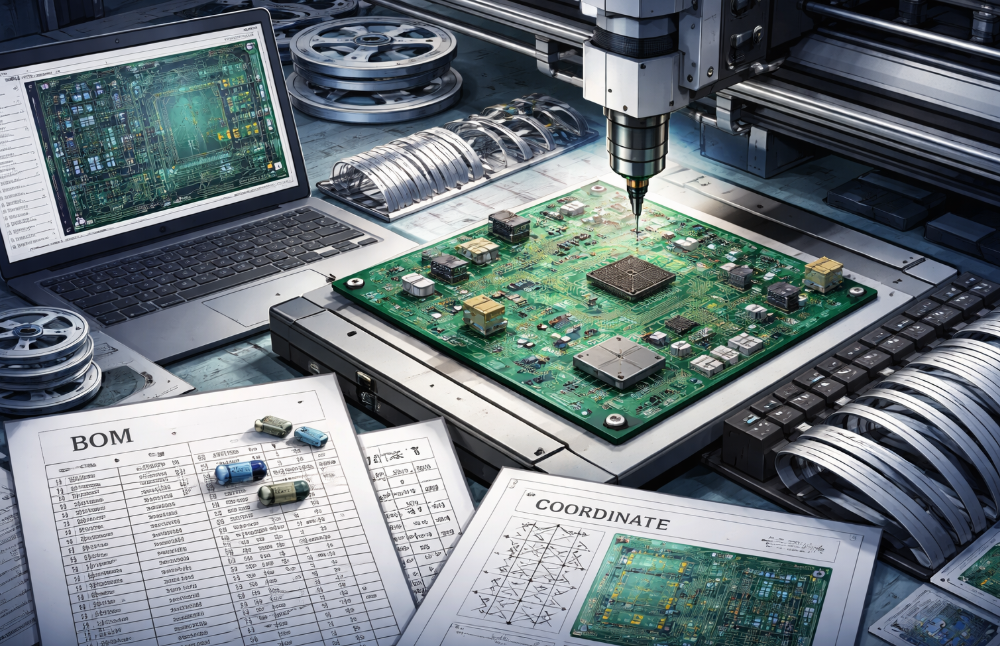
From Concept to Mass Production: The Essential File Checklist and Pitfalls for a Turnkey PCBA Project
In a turnkey PCBA (Printed Circuit Board Assembly) model, customers outsource PCB fabrication, component sourcing, SMT/DIP assembly, testing, and sometimes even packaging to a single manufacturer. While this approach appears to be hassle-free, the quality and completeness of the data provided at the early stage directly determine project cost, lead time, and yield.
In practice, many PCBA projects do not fail due to manufacturing capability, but rather due to incomplete, inaccurate, or ambiguous engineering files.
This article systematically explains: What core files are required to start a turnkey PCBA project? What is the role of each file? Which steps are most prone to errors? The goal is to help you minimize risks before production even begins.
 1. What Is Turnkey PCBA and Why File Preparation Matters More Than You Think
Turnkey PCBA is not simply “sending files and waiting for finished boards.” It is a data-driven engineering process. Without continuous clarification of design intent, manufacturers must rely entirely on the documents you provide to complete:
- PCB fabrication parameter confirmation
- Component selection and procurement
- SMT/DIP programming and soldering
- Testing strategy and quality control
Any ambiguity in the files will be amplified into manufacturing risks.
2. Core Files Required to Start a Turnkey PCBA Project
2.1 Bill of Materials (BOM) – The Core of a Turnkey Project
The BOM is far more than a simple component list. It is the central link connecting design, procurement, and production.
Key information that must be included in the BOM
- Reference designators
- Component description
- Manufacturer Part Number (MPN)
- Package / footprint
- Quantity per board
- Component grade (commercial / industrial / automotive)
- Alternative parts or AVL information
Common BOM-related mistakes
- Listing parameters only, without MPNs
- Mismatch between reference designators and pick-and-place files
- Multiple MPNs listed without defining primary and alternative options
Recommendation: Always provide a production-ready BOM, not a simplified design-stage BOM.
 2.2 Gerber Files – The Only Basis for PCB Fabrication
Gerber files determine whether the PCB is manufactured correctly, not just whether it can be manufactured at all.
A standard Gerber package should include
- Copper layers (Top / Bottom / Inner layers)
- Solder mask layers
- Silkscreen layers
- NC drill files
- Board outline / profile
Typical Gerber issues
- Missing or unclear board outline
- Solder mask openings not aligned with pads
- Multiple Gerber versions provided without clear final labeling
Recommendation: Provide a single folder clearly marked as “Final Release” to avoid version confusion.
2.3 Pick & Place File – The Key to Accurate SMT Assembly
The pick-and-place (coordinate) file is used by SMT machines to identify component locations and orientations.
Required information in the coordinate file
- Reference designator
- X / Y coordinates
- Rotation angle
- Side (Top / Bottom)
- Unit (mm or mil)
High-frequency errors
- Undefined origin point (board center vs. lower-left corner)
- Rotation definitions incompatible with factory equipment
- Bottom-side components omitted
2.4 Assembly Drawing – The “Instruction Manual” for Engineers
Assembly drawings help manufacturing engineers understand special assembly requirements that may not be obvious from Gerber or coordinate files.
Recommended contents of an assembly drawing
- Clearly labeled reference designators
- Polarity and orientation markings
- Enlarged views of critical components
- Notes for manual soldering or special processes
Commonly overlooked problems
- Polarity-sensitive components without clear orientation indicators
- Assembly drawings inconsistent with the final Gerber data
2.5 Schematic – A Valuable Reference for Engineering Review
While not always mandatory, schematics are extremely helpful in the following cases:
- First-time production of a new design
- High-density designs using BGA or QFN packages
- Functional issues requiring engineering support
Schematics enable faster DFM, DFA, and troubleshooting during testing.
2.6 Test Files and Test Requirements
If you expect the manufacturer to take responsibility for functional quality, simple power-on inspection is not sufficient.
Useful test-related documentation
- Test point definitions
- ICT or FCT test instructions
- Fixture requirements
- Pass/fail criteria
 3. The Most Error-Prone Stages in Turnkey PCBA Projects
3.1 Inconsistency Between BOM and Pick & Place Files
This is one of the most common and most serious issues, often leading to wrong or missing components during assembly.
3.2 Ignoring Component Availability
A component that is valid at the design stage may not be available for mass production. Shortages, long lead times, or EOL parts can severely impact schedules.
3.3 Poor File Version Control
Multiple revisions without clear version numbering are a major source of engineering mistakes.
3.4 Special Process Requirements Not Communicated in Advance
Examples include:
- Selective soldering
- Nitrogen reflow
- Manual soldering ratios
4. How to Deliver a Turnkey PCBA Project Correctly the First Time
- Create a standardized file checklist
- Apply consistent version numbers and release dates to all files
- Conduct a DFM/DFA review before placing the order
- Proactively communicate design priorities and risk points
 5. Professional Turnkey PCBA Starts with Professional Documentation
Turnkey PCBA does not eliminate complexity—it manages complexity through high-quality engineering data. When your files are clear, complete, and production-oriented, manufacturers can fully leverage their manufacturing and supply chain capabilities.
If you are planning to launch a turnkey PCBA project, start by reviewing your BOM, Gerber, and pick-and-place files. This single step often determines 80% of the project’s success.
Leave A Comment