

The color of a PCB (Printed Circuit Board) not only affects the product’s appearance but can also influence manufacturing processes, ease of inspection, and overall performance. Choosing the right PCB color is a crucial decision in design and production. This article explores the advantages and disadvantages of different PCB colors, their applications, solder mask characteristics, silkscreen combinations, and why green PCBs remain the most popular choice. This will help engineers and procurement professionals make the best decision.
I. Importance of PCB Color
1. Composition of PCB Color
The color of a PCB is primarily determined by its solder mask, which covers the copper traces to prevent short circuits, oxidation, and corrosion. The silkscreen layer is used for component markings and reference information, typically in white or black.
2. Impact of Color on PCB Manufacturing and Applications
- Production Cost: Different solder mask colors vary in price. Green is the most cost-effective, while special colors are more expensive.
- Automated Optical Inspection (AOI): Some colors, such as black and white, can reduce AOI accuracy.
- Visibility and Maintenance: Color affects the readability of circuit traces, impacting ease of repair.
- Heat Dissipation: Different colors absorb heat differently, affecting the PCB’s cooling efficiency.
II. Advantages and Disadvantages of Different PCB Colors
1. Role of the Solder Mask
The solder mask serves several functions:
- Protecting Copper Traces: Prevents oxidation, short circuits, and electrochemical corrosion.
- Reducing Solder Bridging: Improves soldering reliability.
- Enhancing Visibility: Assists in component placement and circuit inspection.
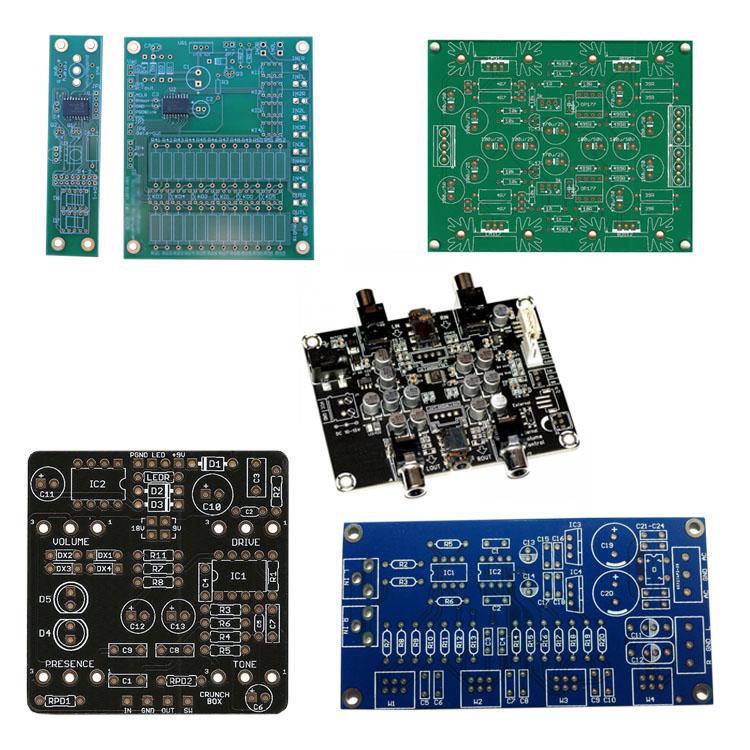
2. Analysis of Common PCB Colors
- Green PCB: The most common choice due to mature manufacturing processes, low cost, and optimal AOI performance. However, it is visually standard and may not be suitable for unique brand identification.
- Black PCB: Premium appearance, commonly used in high-end electronics and gaming devices. However, it has poor heat dissipation and makes circuit inspection difficult.
- Red PCB: High contrast and excellent heat resistance, making it ideal for automotive electronics and high-end PCBs. However, it has a higher production cost.
- Blue PCB: Offers high contrast and is suitable for high-precision circuits in aerospace, medical, and computing applications. Though slightly more expensive than green, its superior visibility makes it widely used in specific industries.
- Yellow PCB: Highly distinguishable and used in applications requiring high visibility. However, it is less commonly available, leading to supply chain limitations.
- White PCB: Due to its excellent reflectivity, it is widely used in LED lighting and signage. However, it easily gets dirty and is difficult to inspect.
- Purple PCB: A customized option that provides strong brand identity. However, it is more expensive and less available, making it primarily used for high-end custom PCB designs.

III. Characteristics and Selection of PCB Solder Mask
1. Solder Mask Thickness and Durability
Different solder mask colors may have variations in thickness, affecting chemical resistance, abrasion resistance, and soldering quality.
2. Impact of Color on High-Frequency Signals
The dielectric constant (Dk) of the solder mask influences signal integrity, and high-speed PCB designs must consider color effects on signal loss.
3. Environmental Adaptability
- High-Temperature Conditions: Red and green PCBs perform more stably.
- High-Humidity Conditions: Blue and black PCBs may absorb more moisture and require additional treatment.
- Chemical Resistance: Green and red solder masks offer superior resistance to chemicals.
IV. PCB Silkscreen Selection and Optimization
1. Standard Silkscreen Color Combinations
- Green PCB→ White silkscreen (best contrast)
- Black PCB→ White or yellow silkscreen (optimized readability)
- White PCB→ Black silkscreen (enhanced contrast)
- Blue/Red PCB→ White silkscreen (clear visibility)
2. Impact of Silkscreen Material on Durability
High-quality silkscreen ink provides abrasion resistance and high-temperature stability, preventing wear and ensuring longevity, which is essential for industrial and long-term PCB use.
V. Why Are Most PCBs Green?
1. Historical Development of Green PCBs
Green was the first standardized PCB color due to its mature production process and widespread adoption.
2. Manufacturing Advantages of Green PCBs
- Lowest Cost: Green solder mask is the most common, making mass production cheaper.
- Optimal AOI Compatibility: Green provides moderate contrast, making it easier to detect circuit defects.
- Eye Comfort: Green is easier on the eyes for long inspection sessions compared to other colors.
3. Process Compatibility of Green PCBs
Green solder mask has high chemical stability, making it suitable for various PCB substrates. It also performs well in heat resistance and chemical corrosion protection.

VI. Conclusion: How to Choose the Best PCB Color?
1. Key Factors to Consider in PCB Color Selection
- Manufacturing Process: Green is the most mature, while black and white may impact inspection.
- Application Scenario: High-end electronics may prefer black; medical devices may require blue.
- Repairability: Green and red are easier to inspect, while black makes repairs more difficult.
- Branding and Aesthetics: Custom colors (purple, gold) are used for high-end branding.
2. Decision-Making Recommendations Before Production
Before finalizing a PCB color, it is recommended to:
- Confirm production feasibility and supply chain stability with manufacturers.
- Consider thermal management, durability, and ease of maintenance.
- Choose a color that meets industry standards to reduce production costs.
The choice of PCB color is not just about aesthetics; it involves manufacturing, cost, inspection, and application suitability. Green remains the most optimal choice, but depending on specific requirements, red, blue, black, and other colors may be better suited for certain applications. This guide aims to help engineers and procurement professionals make informed PCB color choices.
Leave A Comment