
Choosing a PCB might seem straightforward, but in practice, it’s like navigating through a maze. Single-sided, double-sided, multi-layered — just hearing these terms might leave you a little confused. Add in materials, processes, and use cases, and it’s easy to feel lost. As the soul of an electronic project, the choice of PCB impacts not only the product’s performance but also directly affects your budget and project timeline. So, how can you choose the PCB that’s best for you while avoiding common pitfalls? Let’s dive into how to make the most informed decision.

1. Understand Your Application Needs
The key to selecting the right PCB is clearly understanding your application needs. The operating environment, electrical performance requirements, and physical constraints directly influence whether the PCB type and design are compatible with your real-world use.
Key factors to consider:
Operating Environment:
Temperature Range: High or low temperature environments (e.g., automotive electronics, industrial equipment) require PCBs with strong heat resistance.
-
- Humidity & Waterproofing: Humid environments may require special coatings or waterproofing treatments.
- Chemical Exposure: Medical or chemical equipment demands PCBs with high corrosion resistance.
Electrical Performance Needs:
Signal Transmission Speed: High-speed signal transmission requires high-frequency PCBs (e.g., 5G devices).
-
- Current Capacity: High-power devices (e.g., power management systems) need thick-copper PCBs.
- Electromagnetic Compatibility (EMC): Some applications require special designs to reduce electromagnetic interference (e.g., communication devices).
Physical Design Requirements:
Size and Shape: Portable devices require smaller, more complex multi-layer boards.
-
- Flexibility: Wearable or dynamic components often need flexible or rigid-flex PCBs.
- Thickness and Weight: Aerospace, drones, etc., require strict limitations on weight and thickness.
Reliability & Longevity:
Usage Lifespan: Medical, aerospace, etc., require long-lifetime, high-reliability PCBs.
-
- Vibration Resistance: Automotive and industrial applications require vibration-resistant designs.
Cost Considerations:
Balancing cost and performance for mass production is crucial in selecting the right PCB.
Regulatory Compliance:
Different industries have varying quality and safety requirements for PCBs. Make sure you understand the applicable regulations to ensure your product meets certification standards, avoiding unnecessary risks.
2. PCB Types and Their Applications
PCBs are not one-size-fits-all; different types of materials and designs are suited to different applications. Common PCB types include:
Single-sided PCBs:
Features: Circuitry is arranged on one side, simple design, low manufacturing cost.
Applications: Suitable for simple electronic devices, such as small household appliances and toys.
Double-sided PCBs:
Features: Circuitry is arranged on both sides, providing more connection options and design flexibility.
Applications: Used in more complex devices, such as TVs, sound systems, etc.
Multi-layer PCBs:
Features: Contains three or more circuit layers, suitable for high-density designs.
Applications: Widely used in high-performance electronic products, such as smartphones, computers, etc.
Flexible PCBs:
Features: Can bend, suitable for space-constrained or flexible designs.
Applications: Used in smartwatches, wearable devices, etc.
Rigid-flex PCBs:
Features: Combines rigid and flexible properties to meet various installation needs.
Applications: Common in medical devices, aerospace, etc.
High-frequency PCBs:
Features: Optimized materials and designs for high-frequency signal transmission.
Applications: Widely used in communication devices, radar systems, etc.
Aluminum-based PCBs:
Features: Excellent heat dissipation, suitable for high-power applications.
Applications: Common in LED lighting, power modules, etc.

3. Choosing the Right PCB Materials for Optimal Performance
The choice of PCB materials has a significant impact on performance, reliability, and cost. Understanding the characteristics of different materials helps make the right selection during the design phase.
Common PCB Materials:
FR-4 (Fiberglass Epoxy Resin):
Features: Most common PCB material with good mechanical strength, electrical properties, and heat resistance, moderately priced.
Applications: Widely used in consumer electronics, computers, communication devices, home appliances, etc.
CEM-1 (Paper-based Epoxy Resin):
Features: Made from paper-based material and epoxy resin, cost-effective, suitable for low-end applications.
Applications: Primarily used in low-cost electronics like simple appliances, lighting systems, etc.
High-frequency Materials (e.g., PTFE):
Features: Excellent electrical performance, particularly for high-frequency signal transmission.
Applications: Used in communication devices, radar systems, satellite communications, 5G devices, etc.
Aluminum-based Materials:
Features: Made from aluminum, providing excellent heat dissipation, suitable for high-power applications.
Applications: Widely used in LED lighting, power amplifiers, power management systems, etc.
Polyimide (PI) Materials:
Features: High heat resistance and flexibility, suitable for extreme environments.
Applications: Common in flexible PCBs, rigid-flex PCBs, and high-end medical devices, aerospace electronics, etc.
Ceramic Materials:
Features: Excellent thermal conductivity, electrical performance, and mechanical strength, used in high-precision and stable applications.
Applications: Used in high-frequency, high-power, and high-stability devices like aerospace, military, medical equipment, etc.
Paper-based Materials:
Features: Low cost, suitable for simple circuits but lacks the durability and performance of other materials.
Applications: Common in low-end consumer electronics and toys.
4. Choosing a Manufacturer: Key Factors for Ensuring Quality
Choosing a reliable PCB manufacturer is crucial to ensuring the quality, reliability, and long-term stability of the product. A good manufacturer will provide not only high-quality PCBs but also guarantees throughout the production process.
Factors for Reliable Manufacturers:
- High-quality Raw Materials: Manufacturers using high-quality materials ensure the PCB’s reliability and longevity.
- Advanced Production Processes: High-level production techniques guarantee circuit board precision and stability.
- Strict Quality Control: Ensures each PCB meets quality standards, reducing defects and rework.
- Quick Response & Flexibility: A reliable manufacturer responds promptly to customer needs and adjusts production schedules to ensure timely delivery.
- Long-term Partnership: Manufacturers with long-standing customer relationships tend to offer consistent quality and service.
- Comprehensive After-sales Service: Efficient after-sales support helps resolve any issues that may arise during use.
JiaYuan Technology: Your Reliable Quality Partner
As an experienced PCB manufacturer, JiaYuan Technology places a strong emphasis on quality. We use the best raw materials, adopt advanced production processes, and implement strict quality control to ensure that every PCB meets industry standards. Additionally, we offer flexible customization services and comprehensive after-sales support, providing customers with the most efficient and reliable solutions. Choosing JiaYuan Technology means choosing a trustworthy partner with guaranteed quality.
5. Advanced Design Considerations
In the PCB design process, it’s crucial to ensure that the design meets both functional and performance requirements.
Key Design Factors:
- Impedance Control: For high-speed signal applications, impedance control is a vital design consideration.
- Thermal Management: Effective heat dissipation is essential to prevent performance degradation from overheating.
- Layer Stacking: Proper layer stacking design optimizes PCB performance and reduces signal interference.
- Panelization: Panelization design can reduce production costs but requires careful planning to avoid losses.
6. Testing PCBs
There are various methods for testing PCBs, ranging from visual inspection to electrical verification. Each testing method serves a specific purpose to ensure product quality and reliability.
Common Testing Methods:
Visual Inspection: Examining the PCB visually or under magnification to check for visible defects, such as faulty solder joints or traces.
Application: Used for simple inspections, often in the initial stages of production.
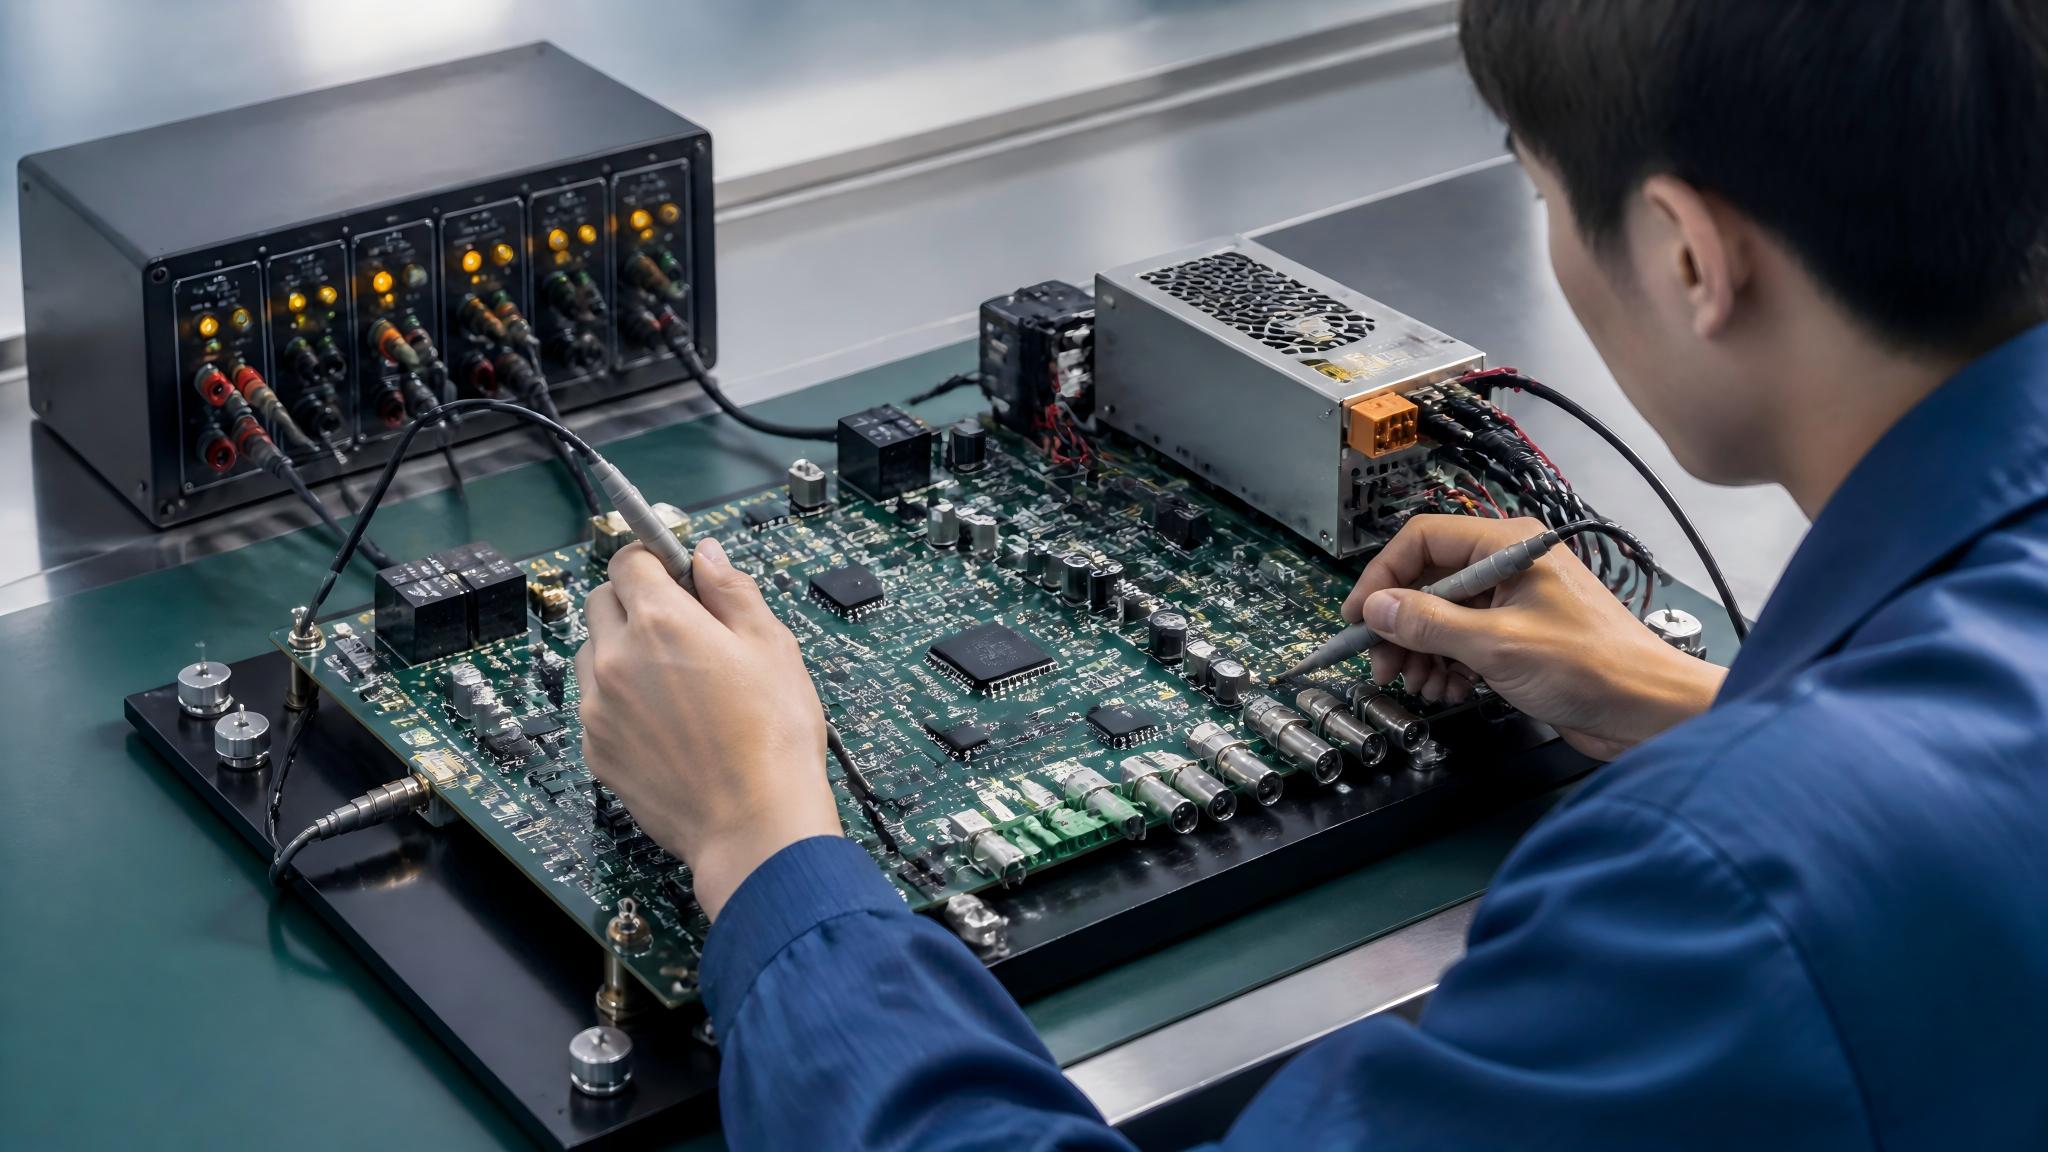
Flying Probe Testing: Using multiple movable probes to directly contact the PCB’s solder points for electrical testing.
Application: Suitable for small-batch production or complex PCBs, effectively detecting shorts, open circuits, and component failures.
Automatic Optical Inspection (AOI): Using high-speed cameras to scan the PCB’s surface and detect defects like misplaced components or solder joint issues.
Application: Widely used in medium-to-high-end production lines to automatically detect and locate defects.
Electrical Testing: Testing the electrical performance of the circuit (e.g., resistance, current, voltage) to confirm if the PCB meets design specifications.
Application: Used to ensure the PCB’s electrical connections are reliable.
In-Circuit Testing (ICT): After component assembly, specialized testing equipment checks each component to ensure proper operation and conformance to design.
Application: Commonly used in mass production to test component soldering, open circuits, shorts, etc.
X-ray Inspection: Using X-rays to scan the PCB, checking solder joints, internal circuitry, and layer-to-layer connections, especially useful for multi-layer boards and surface-mount technology (SMT).
Application: Widely used for high-density, multi-layer PCBs and 3D solder joint inspection.
Functional Testing: Connecting the fully assembled PCB to power and simulating its actual operating environment for functionality testing.
Application: Used to verify if the PCB operates as designed, especially for final product validation.
Environmental Testing: Testing the PCB in extreme environmental conditions like high or low temperatures, humidity, etc., to evaluate its performance under harsh conditions.
Application: Suitable for high-end devices, particularly in automotive, aerospace, and medical sectors.
Burn-in Testing: Running the PCB for extended periods while simulating real-world loads to detect potential failures and instability.
Application: Primarily used for high-reliability products like military and aerospace devices.

7. Cost and Time Management
In large-scale production, balancing cost and quality is essential. Ensuring quality while controlling costs will lead to efficient and economical production.
Cost Factors:
- PCB type and material selection
- Design complexity (e.g., number of layers, microvia usage)
- Production volume (prototype vs. mass production)
Time-saving Tips:
- Use manufacturers with rapid turnaround capabilities for quick prototyping.
- Communicate your requirements clearly to avoid delays.
Choosing the right PCB is not a task to be taken lightly. It requires a comprehensive understanding of application needs, design requirements, material choices, and manufacturer evaluation. By understanding the characteristics and application scenarios of different types of PCBs, you can make more informed decisions and ensure that your project achieves the best balance of quality and cost.
Our Team
Leave A Comment