
How to Create an Error-Free BOM for Custom PCB Assembly
In a custom pcba project, the BOM is more than a parts list. It connects design data with production data. A reliable BOM should include reference designators, manufacturer part numbers, complete specifications, packages, brands, alternate rules, life-cycle status, MSL information, quantities, and material requirements. The BOM should also match the Gerber files, placement data, assembly drawings, and test documents. This alignment helps quoting, purchasing, IQC, kitting, assembly, inspection, and traceability teams use the same data.
A wrong package may not fail during the quote stage. Purchasing may order the wrong part. IQC may miss the mismatch. Kitting may mix similar components. The error may appear later during SMT assembly or functional testing. An error-free BOM does not need more words. It needs clear data that every downstream team can execute.
A good BOM supports every production handoff. The sections below follow the way a PCBA factory uses BOM data. They explain common risks and practical checks. They also show how to submit Gerber files and a BOM for a more accurate custom PCBA quote.
1. A BOM Is a Production Interface, Not Just a Parts List
1.1 Who Reads the BOM Inside a PCBA Factory?
Several teams use the same BOM during a custom PCB assembly project. Quoting staff use it to estimate material cost and assembly scope. Buyers use it to confirm manufacturer part numbers, brands, and supply status. Warehouse staff use it to receive and kit material. SMT engineers use it to prepare feeder and loading data. Quality teams use it to check incoming material and process records. Test teams use the BOM revision to confirm test conditions.
The BOM therefore serves more than the design team. It links quoting, purchasing, warehousing, production, quality, and service records. Engineers may write a BOM for design review. Production teams need a BOM that supports clear execution. A strong custom pcba BOM uses consistent fields and naming rules across every department.
1.2 The Field Groups an Interface-Level BOM Needs
Reference designators should remain unique. They should match the PCB silkscreen, assembly drawing, and placement file. The manufacturer part number, or MPN, should use the full original part number. A private short code should not replace the MPN. The description should include values and ratings needed for purchasing. These may include resistance, capacitance, voltage, tolerance, and power.
The brand or AVL field should state the preferred brand and accepted range. The alternate field should separate approved alternates, prohibited alternates, and parts that need engineering approval. The life-cycle field can mark active, end-of-life, or supply-risk parts. Moisture-sensitive parts should include relevant MSL information. Quantity should separate quantity per board, build quantity, and material preparation needs. Notes should cover polarity, orientation, jumpers, programming status, and DNI or DNP requirements.
PCBnet lists manufacturer part number, manufacturer name, quantity, reference designator, package information, alternates, and DNI or DNP status as important BOM data. EMS Technologies also explains that a complete BOM needs usable manufacturer part numbers, not vague descriptions. The final field requirements should follow the customer specification and assembler requirements.
1.3 Where BOM Errors Usually Appear
A wrong package can lead purchasing staff to select a similar part that cannot fit the board. A short description can make different parts look interchangeable. Missing polarity information can confuse SMT programming and AOI review. An old part number can reveal an end-of-life problem only after the purchase request starts.
Missing quantity and material preparation data can make kit completion unclear. Missing package format can prevent reels, trays, tubes, or cut tape from going directly to the line. Missing DNI or DNP notes can cause unwanted installation. A small BOM error can therefore become a purchasing, assembly, testing, or rework risk.
2. Quoting: BOM Completeness Controls Quote Accuracy
2.1 How Quoting Teams Read Price, Quantity, and Package Data
Quoting teams review each BOM line to estimate component cost, purchase quantity, and assembly work. Parts with the same function may differ by brand, package, packaging format, and supply channel. A BOM without brand limits or alternate rules forces the supplier to use assumptions. The quote may change after the customer confirms the actual parts.
The BOM should state whether a line requires one exact part number, allows AVL alternates, or allows supplier suggestions. Long-lead parts, end-of-life risks, and NCNR items should have separate notes. These fields help buyers review cost, inventory, and supply risk before production planning.
2.2 Why Submit Gerber Files and the BOM Together?
Gerber files describe PCB layers, pads, solder mask, silkscreen, drill data, and board outline. The BOM describes the components installed on the board. The placement file provides component coordinates, rotation, and assembly side. The assembly drawing adds polarity, orientation, connector, and special assembly details. These documents need to match each other.
Submitting Gerber files with the BOM lets engineers compare reference designators, packages, and quantities. The placement file adds another check for component position and assembly side. PCBnet recommends Gerber files, a BOM, placement data, assembly drawings, and assembly notes for a PCB assembly quote. Submit the Gerbers, complete BOM, and placement data together to support a practical engineering review and quote.
3. Purchasing: BOM Quality Controls Supply Risk
3.1 Life-Cycle Status and End-of-Life Warnings
A BOM should describe more than the current part selection. It should also show life-cycle risk. Active parts can follow normal purchasing review. End-of-life parts need inventory and alternate planning. PCN changes may affect electrical parameters, package details, or supply channels. Long-lead parts need early purchasing feedback.
Mark end-of-life risk, long-lead status, single-source status, and customer-owned parts in the BOM. Small builds still need this information. A few constrained parts can stop a complete production plan. The supplier can use these notes to report purchasing limits. The customer engineering team should approve any final part change.
3.2 Alternate Parts and AVL Rules: State What Can Change
Alternate management should separate allowed and prohibited substitutions. An allowed alternate should include the accepted brand, alternate part number, and approval condition. A prohibited alternate should carry a controlled-part note. Critical chips, sensors, connectors, and programmed parts may need a stricter review.
Automotive electronics, medical equipment, and industrial control projects may need validation and approval records for alternates. The BOM should state who approves the change, when approval applies, and where the record stays. A supplier suggestion does not equal product approval. The final decision should follow engineering data and project quality requirements.
3.3 Attrition, Purchase Timing, and NCNR Material
Material requirements should not use one fixed loss rate for every component. Package type, packaging format, assembly process, build quantity, and supplier rules can change the requirement. The BOM can state a line-specific material requirement. The customer can also ask the assembler to confirm replenishment and leftover rules during quoting.
NCNR parts, long-lead parts, and special-order material need clear notes. Purchasing staff can use these notes to plan the order sequence. The customer should also confirm ownership, storage, and return rules for unused material. Clear rules reduce inventory disputes at project close.
4. IQC: The BOM Sets the Incoming Inspection Reference
4.1 How IQC Checks Brand, Part Number, Lot, and Packaging
IQC teams usually compare incoming material with the BOM. They may check part number, brand, specification, quantity, lot, and package format. Clear BOM data makes this check easier. Vague descriptions force inspectors to rely on experience. That approach increases the risk of mixed or wrong material.
Moisture-sensitive devices also need storage and moisture-control information. MSL data should appear in the BOM or related material documents. ESD-sensitive parts need the correct handling procedure. The exact inspection and handling method should follow device data, customer standards, and supplier procedures.
4.2 BOM Roles in Turnkey, Consigned, and Hybrid Builds
In a turnkey build, the supplier usually checks purchased parts against the purchase order and BOM. In a consigned build, the customer supplies complete, identifiable, and usable material. In a hybrid build, the BOM should mark customer-supplied and supplier-sourced lines separately.
A supplier may check customer material for quantity, part number, packaging, and appearance. Component performance, source, and authenticity duties depend on the contract and inspection scope. IQC is an important control point. It does not automatically assign every responsibility to one party. The project documents should define the boundary.
5. Kitting: Match the BOM to the Feeder List
5.1 Reference Designators and Mixed-Brand Risks
Kitting converts BOM data into a material list, feeder list, and loading information. Each reference designator should remain unique. It should match the PCB silkscreen. The same resistance value does not make every resistor interchangeable. Temperature coefficient, tolerance, power, and voltage rating may affect actual use.
A BOM should not only say “resistor,” “capacitor,” or “connector.” It needs data that purchasing and warehouse teams can verify. The notes should identify parts or lots that cannot mix. Clear restrictions help warehouse and production teams reduce material mix-ups.
5.2 How to State Kit Quantity, Attrition, and Leftover Rules
Before kitting, the supplier needs build quantity, quantity per board, and preparation requirements. Reels, tubes, trays, and cut tape can affect loading. Packaging format can also affect leftover records and return handling. The customer should confirm these rules during the quote stage.
The BOM or related kitting list should state customer-supplied material, supplier-sourced material, replenishment, and leftover handling. The exact preparation rule depends on the component, process, and assembler. Avoid using a generic attrition figure without project support.
6. SMT and THT: Control Polarity, Orientation, and Revision
6.1 The BOM, Gerber, and Placement File Cross-Check
The placement program usually uses centroid data. The stencil and PCB fabrication data come from Gerber files. The loading list and material checks depend on the BOM. A revision mismatch can cause wrong placement, reverse placement, missing placement, or failed verification.
After every ECO or design revision, update the BOM, Gerber files, placement data, and assembly drawing together. Use one clear revision reference. Check designators, packages, quantities, and assembly sides before production. First article approval should use the latest aligned data set.
6.2 Polarity, IC Orientation, and ECO Changes
Electrolytic capacitors, diodes, LEDs, and some connectors need clear orientation data. IC pin one also needs a clear relation to the package direction. BOM notes, assembly drawings, silkscreen, and placement data should agree. Production staff should not guess when documents conflict.
After an engineering change, update the feeder list, placement program, and test documents. The line should use the approved BOM revision. Repair teams should also confirm the original revision before retesting a board. This control prevents mixed-revision production.
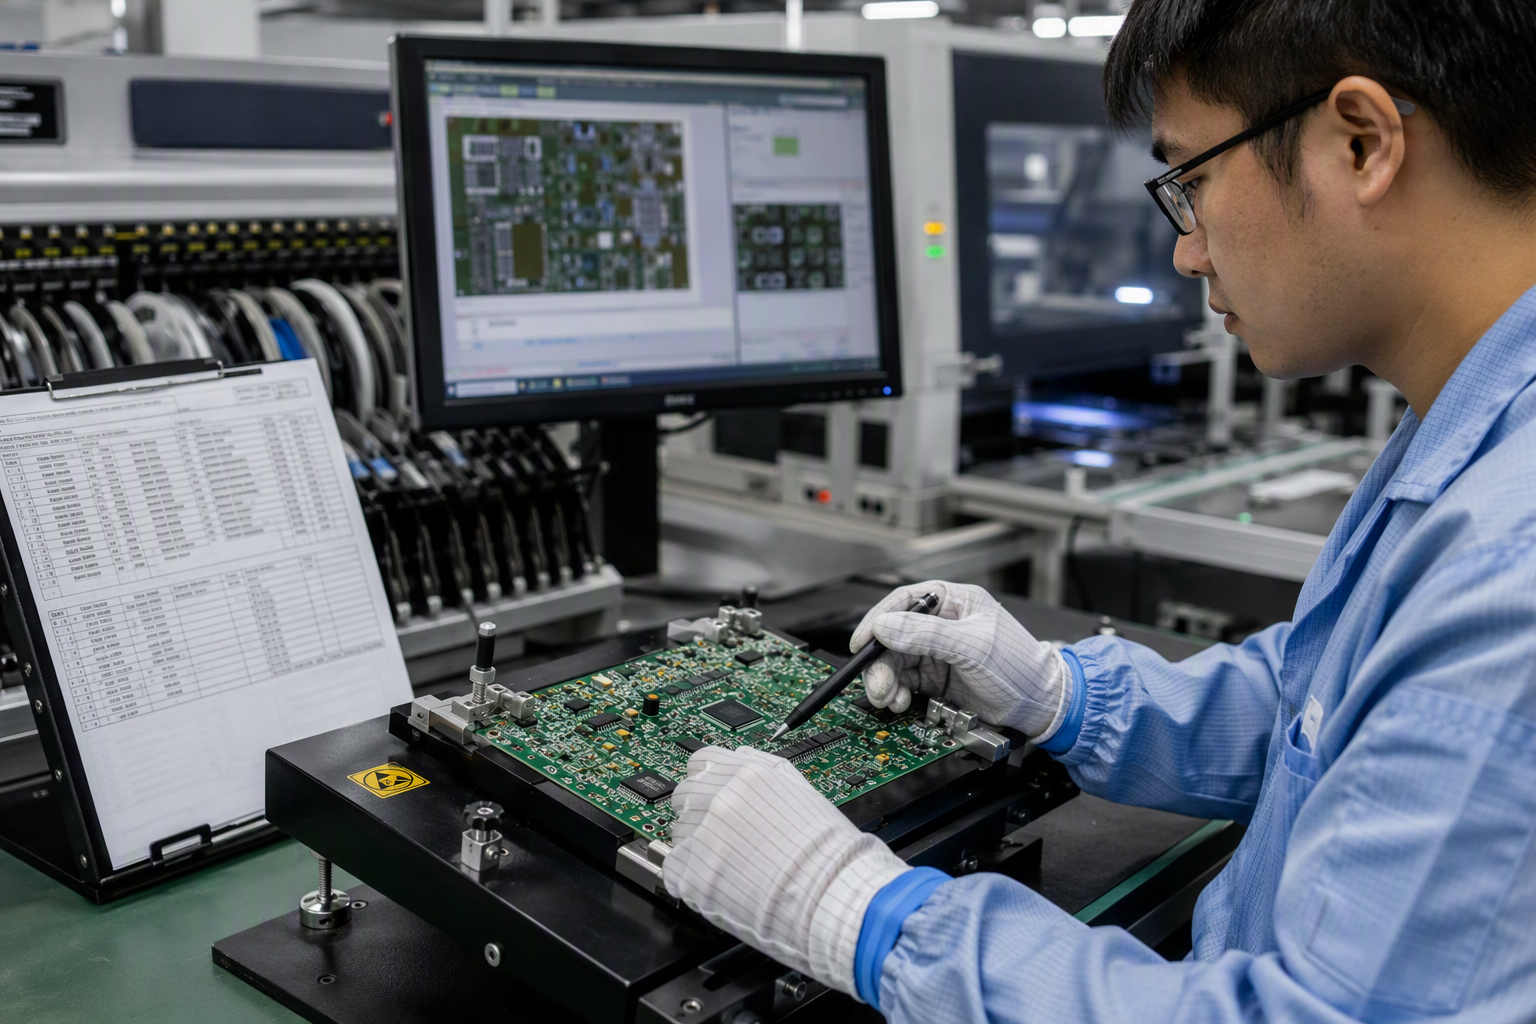
7. AOI and X-Ray: Inspection Programs Use BOM Data
7.1 How AOI Uses the BOM and Placement Data
AOI programs often use the BOM, placement data, and assembly documents. Inspection may cover wrong parts, missing parts, polarity, offset, and visible solder defects. Reference designators and package information influence the inspection logic.
When the BOM changes, the AOI program and decision rules need review. Otherwise, the line may use new material while the inspection program checks the old revision. The final inspection plan should match product requirements and available inspection capability.
An error-free BOM connects quoting, purchasing, kitting, SMT placement, AOI, and later quality review. Its value comes from consistent fields, clear alternates, accurate packages, and aligned revisions. These checks reduce clarification and rework risk in custom pcba projects.
Conclusion
Submit your Gerber files, complete BOM, placement data, and assembly drawings for a project-based review and quotation. The final scope should follow the actual parts, quantities, processes, and customer requirements.


Leave A Comment