
pcb smt Technology Trends: Improve PCBA Quality and Delivery
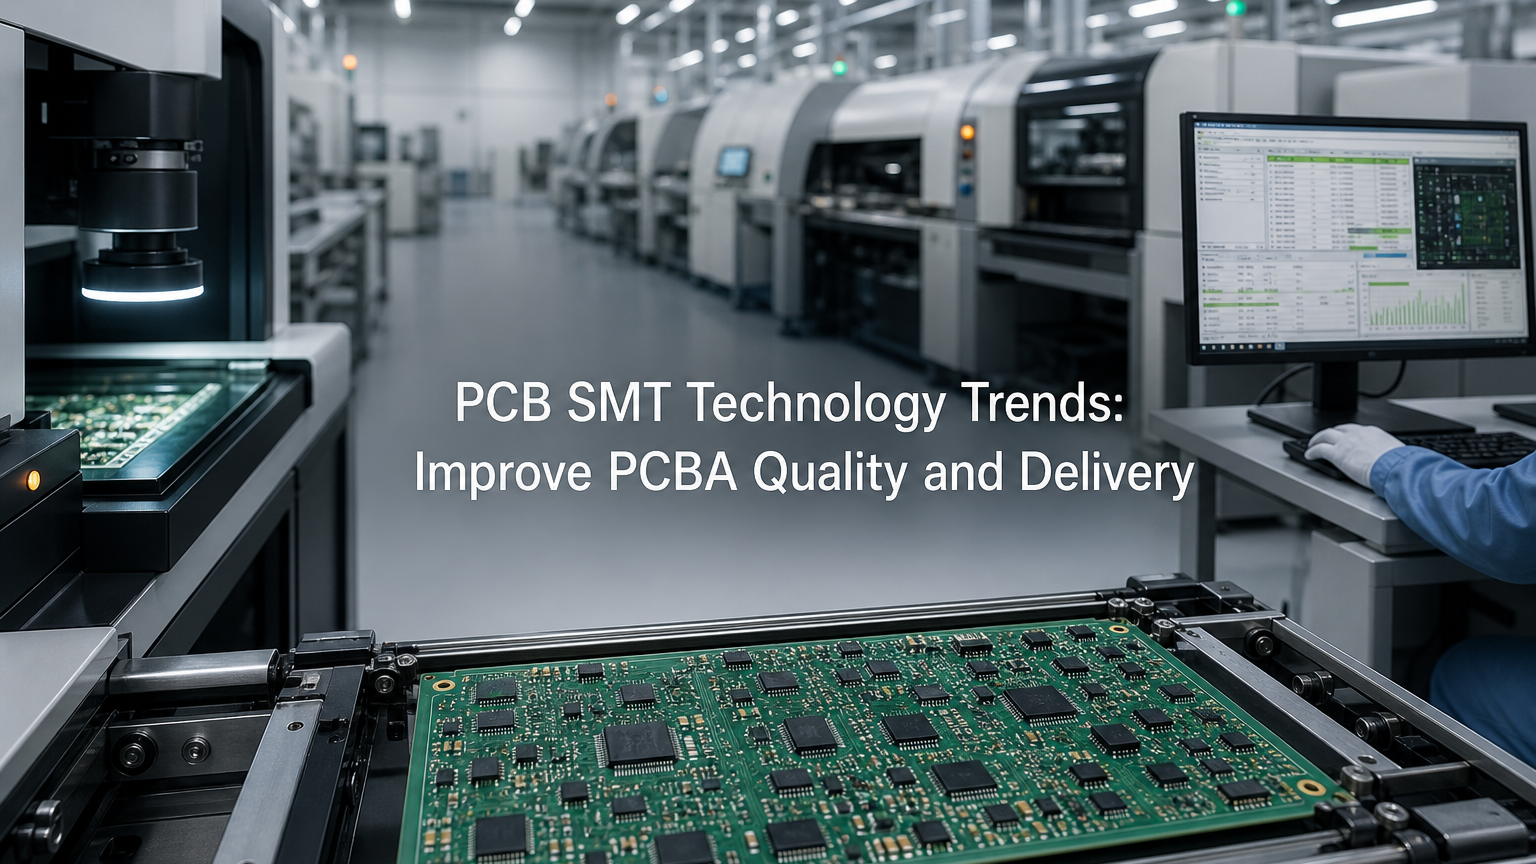
In pcb smt projects, progress means more than faster placement. It also means smaller components, smarter inspection, better data, and stronger traceability. High-density packages increase the need for SPI, AOI, and X-ray inspection. Smart production connects equipment through software. Faster product cycles also make NPI, DFM, and revision control more important. This article explains how these trends affect PCBA production and supplier selection.
1. Improve Inspection with SPI, AOI, and X-Ray
1.1 Manage Solder Paste for Miniature Components
01005 parts, fine-pitch QFPs, BGAs, and QFNs increase printing risks. Small paste errors can affect solder joints. SPI checks paste position, area, height, volume, and shape. Engineers can use these results to adjust stencil openings, squeegee settings, and printing parameters. The required inspection level depends on the smallest component, pad design, stencil, and product risk.
High-density boards also create tighter spacing and pad constraints. DFM review should check packages, pads, stencil openings, and nearby components. This review can reduce placement shifts, bridging, and insufficient solder. SPI does more than find defects. It also reveals printing trends.
1.2 Connect AOI with More Production Data
AOI checks wrong parts, missing parts, polarity, offsets, and visible solder defects. Modern data systems can connect AOI results with the BOM, placement data, placement settings, and reflow profiles. Engineers can then see whether defects cluster around a part, location, or production lot.
AOI programs must match the product revision. A BOM change requires a review of inspection rules. Otherwise, the line may use new material with an old inspection program. Ask suppliers how they control false calls, missed defects, and program revisions.
1.3 Use X-Ray to Protect Hidden Solder Joints
BGA, QFN, and LGA packages contain joints that are difficult to inspect by sight. X-ray inspection can support checks for voids, bridges, and internal joint conditions. The need for X-ray depends on package structure, product reliability, customer standards, and failure risk.
Inspection equipment cannot define quality by itself. Engineers should also review pad design, the reflow window, and acceptance criteria. Avoid fixed inspection coverage or zero-defect claims. Build the inspection plan around the actual package and quality class.

2. Make Production Smarter with Process Control
2.1 Connect Printing, Placement, and Inspection Data
Smart SMT production does not mean a completely unmanned line. A more practical trend is connected data. SPI results show printing conditions. AOI results reveal placement and soldering trends. Reflow profiles add thermal information to the same review.
When several processes use the same work order, board number, and program revision, engineers can locate the source of an issue faster. The cause may involve paste, stencil, placement settings, or the reflow profile. Data links help teams act during production instead of waiting for batch rework.
2.2 Use MES to Connect Equipment and Quality Records
MES can connect work orders, equipment status, material lots, program revisions, inspection results, and release records. It can support wrong-material prevention, program checks, and process confirmation. It can also store records needed for customer audits.
IPC materials identify IPC-SMEMA-9851, IPC-HERMES-9852, and IPC-2591 CFX as standards for exchanging production status and process data. Actual connectivity depends on equipment, software, and factory systems. MES cannot solve every quality issue. Data quality and shop-floor discipline still matter.
3. Prepare for Production with NPI and DFM
3.1 Use NPI to Close Pilot-Build Issues Faster
Prototype and pilot projects often change the BOM, Gerber files, placement data, and assembly drawings. NPI should cover document review, material risk feedback, first article approval, defect analysis, and revision control. Speed alone does not define NPI quality. The team must close issues before the next build.
First article review can verify component position, orientation, solder condition, and key process requirements. Pilot records also show defect trends. These records help the engineering team judge production readiness. Prototype revisions should remain aligned with production data.

3.2 Use DFM to Solve Problems Before Quoting
DFM review can cover pad design, stencil openings, component spacing, package direction, test points, panelization, and serviceability. Earlier findings reduce later board changes, rework, and pilot risks. After receiving Gerber files and a BOM, the supplier should report manufacturability risks from the actual data.
A quote should not ignore process conditions. A useful review should address materials, boards, placement, inspection, and testing. Buyers can then understand project risks earlier. Engineers can also correct design issues before production.
3.3 Protect First Article Approval with Revision Control
Fast product changes increase revision risks. After an ECO, customers and suppliers should update the BOM, Gerber files, placement data, assembly drawings, feeder list, placement program, and test conditions. Every document should use a clear revision code.
The line should confirm the actual revision before production. Mixed revisions can cause wrong parts, wrong placement, or test errors. First article approval should use one aligned data set. The exact review scope should match the product and customer requirements.
4. Support High-Mix, Low-Volume Production
4.1 Manage More Product Variants with Flexible Production
Industrial control, medical, automotive, and smart hardware projects often include several models, batches, and design updates. SMT lines must keep material preparation, changeovers, inspection, and traceability stable. Flexible production does not mean every product changes instantly. It means the line matches the board, quantity, components, and process needs.
Small batches also need material mix-up prevention. Feeder lists, feeders, programs, stencils, and nozzles should enter the changeover check. Changeover speed should never be judged without error-proofing. Fast changeovers can increase placement errors without BOM checks and first article approval.

4.2 Match the Line to the Order and Process
Prototype, low-volume, and volume orders need different equipment, inspection depth, staffing, and scheduling. During quotation, provide the quantity range, product models, update plan, key packages, and test requirements. The supplier can then assess the right line and process.
Equipment count alone cannot prove delivery capability. Buyers should also review changeover methods, material preparation, program control, inspection coverage, and data records. Flexible production creates value only when it matches real order conditions.
5. Combine Green Processes with High Reliability
5.1 Put Environmental Requirements into Production
Lead-free solder, flux, cleaning materials, waste handling, and energy records may form part of project requirements. RoHS, REACH, and customer material declarations should enter purchasing, IQC, and BOM checks. Environmental control must reach the material and process records.
Lower defect, rework, and scrap levels also improve resource efficiency. SPI, AOI, and process data can reveal printing and placement trends early. Claims about carbon reduction, nitrogen savings, or zero-carbon factories require real data and reliable sources.
5.2 Apply Advanced Packages to High-Reliability Products
Automotive electronics, medical equipment, and industrial controls place more focus on joint reliability, thermal cycling, vibration, hidden joints, and process consistency. BGAs, SiP devices, and other high-density packages may need stronger control of printing, placement, reflow, and X-ray inspection.
Quality classes, test methods, and certifications should follow customer standards, component data, and project documents. An industry trend does not prove that every factory has the same capability. Project evaluation must use real manufacturing data.
6. Protect Quality with Board-Level Traceability
6.1 Link Material Lots with Inspection Records
A traceability chain can start with the BOM and purchasing records. It can then link IQC, kitting, loading, placement, reflow, SPI, AOI, X-ray, functional testing, and shipment serial numbers. Board codes, work orders, and program revisions often support these links. Traceability depth depends on product risk, customer needs, and system capability.
Complete records help teams locate a material lot, production batch, or board after a quality issue. Automotive, medical, and industrial control projects often require strong process records, change records, and test evidence. Ask suppliers whether records can be exported, retained, and searched by board number.

7. Select a PCBA Supplier That Fits Your Project
The supplier should explain how each capability supports the actual product. Ask about key packages, stencil design, SPI, AOI, X-ray, reflow control, and first article review. Equipment models provide useful context. They cannot prove complete line capability alone.
Also review whether the MES or production system can link material lots, BOM revisions, program revisions, board numbers, inspection records, and test results. Small-batch, pilot, and volume builds need different scheduling and process plans. A supplier should assess the project data instead of replacing engineering analysis with a general equipment list.
If your board contains 01005, BGA, QFN, LGA, or other high-density packages, submit Gerber files, a BOM, placement data, and assembly drawings. The engineering team can use these files to review DFM, SPI, AOI, X-ray, and traceability needs. Submit your Gerber files and BOM to request a project-based SMT process review and PCBA quotation. Final pricing, lead time, and service scope should follow the actual project data.
Conclusion
pcb smt technology now connects inspection data, early engineering, flexible production, material compliance, and quality traceability. Submit Gerber files and a BOM to assess your project’s manufacturing readiness.
Leave A Comment