
pcba manufacturing Conformal Coating Process: From Coating Boundaries to Quality Release
In pcba manufacturing projects, conformal coating is more than a surface treatment. It affects moisture protection, electrical insulation, component function, and future repair. A reliable process starts with environmental assessment. It then confirms coating zones, keep-out zones, material status, spray paths, curing conditions, and release criteria.
Direct Answer: PCBA Conformal Coating Process
The PCBA conformal coating process must match the operating environment, component structure, and customer requirements. The basic process includes document review, surface cleaning, masking, coating, curing, demasking, rework, and quality verification. Material type, film thickness, curing method, and test conditions should not use fixed values by default. Final requirements should follow the product TDS, SDS, customer specifications, applicable standards, and actual sample results.
1. Decide Whether the PCBA Needs Conformal Coating
Conformal coating selection should start with product risk. The engineering team first reviews the actual operating environment. It then defines the protection target and coating scope. This sequence helps reduce material selection errors and process rework.
1.1 Identify Coating Risks from the End-Use Environment
Industrial control equipment may face moisture, dust, and temperature changes for long periods. Outdoor equipment may also face condensation, salt spray, and corrosive media. Automotive electronics require attention to vibration, temperature variation, and long-term operation. Medical equipment places more focus on material records, functional stability, and process consistency.
Project documents should therefore describe the operating temperature, humidity, condensation risk, chemical exposure, vibration, and maintenance cycle. These inputs affect material chemistry and coating method. Without clear environmental conditions, the project should not directly specify one conformal coating.
1.2 Define the Protection Target from Product Function
Conformal coating can form an insulating protective film. It can help reduce the impact of moisture, contaminants, and corrosive media on a circuit board. It can also support stable operation in complex electronic assemblies.
However, conformal coating is not a universal waterproof layer. It is not an independent mechanical reinforcement layer. It cannot replace structural sealing or suitable enclosure design. The project should define the protection target before selecting the material and process.
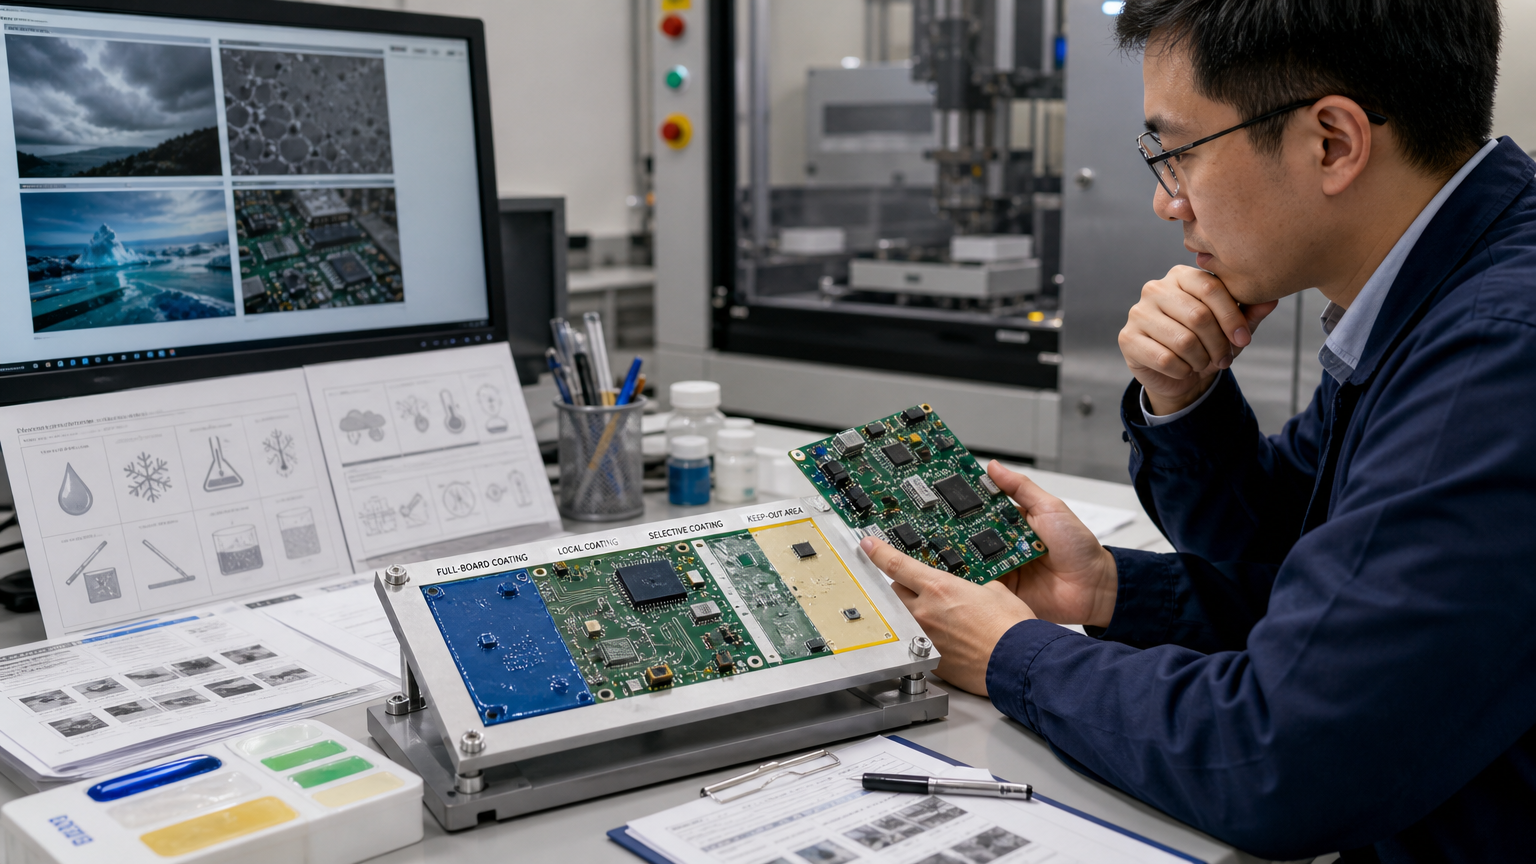
1.3 Decide Between Full, Local, and Selective Coating
Full-board coating may suit products with few keep-out zones. Local coating may suit boards with many sensitive components. Selective coating may suit projects that require precise path and boundary control.
The final method also depends on board complexity, repair needs, and production volume. Not every PCBA should receive full coverage by default. Process documents should clearly identify the coating zones and the areas that must remain free of coating.
2. Define the Coating Boundary: Which Areas Must Stay Clear?
The first practical question in conformal coating is where to apply the material. The coating should not cover every component surface. Some areas must preserve electrical contact, movement, sensing, or heat transfer. A boundary error can create more risk when the spray process itself becomes more stable.
2.1 Connectors, Gold Fingers, Test Points, and Contact Areas
Connector contact surfaces must remain clean. Gold fingers must retain electrical contact. Test points must remain accessible. Terminal areas must also remain free of material contamination.
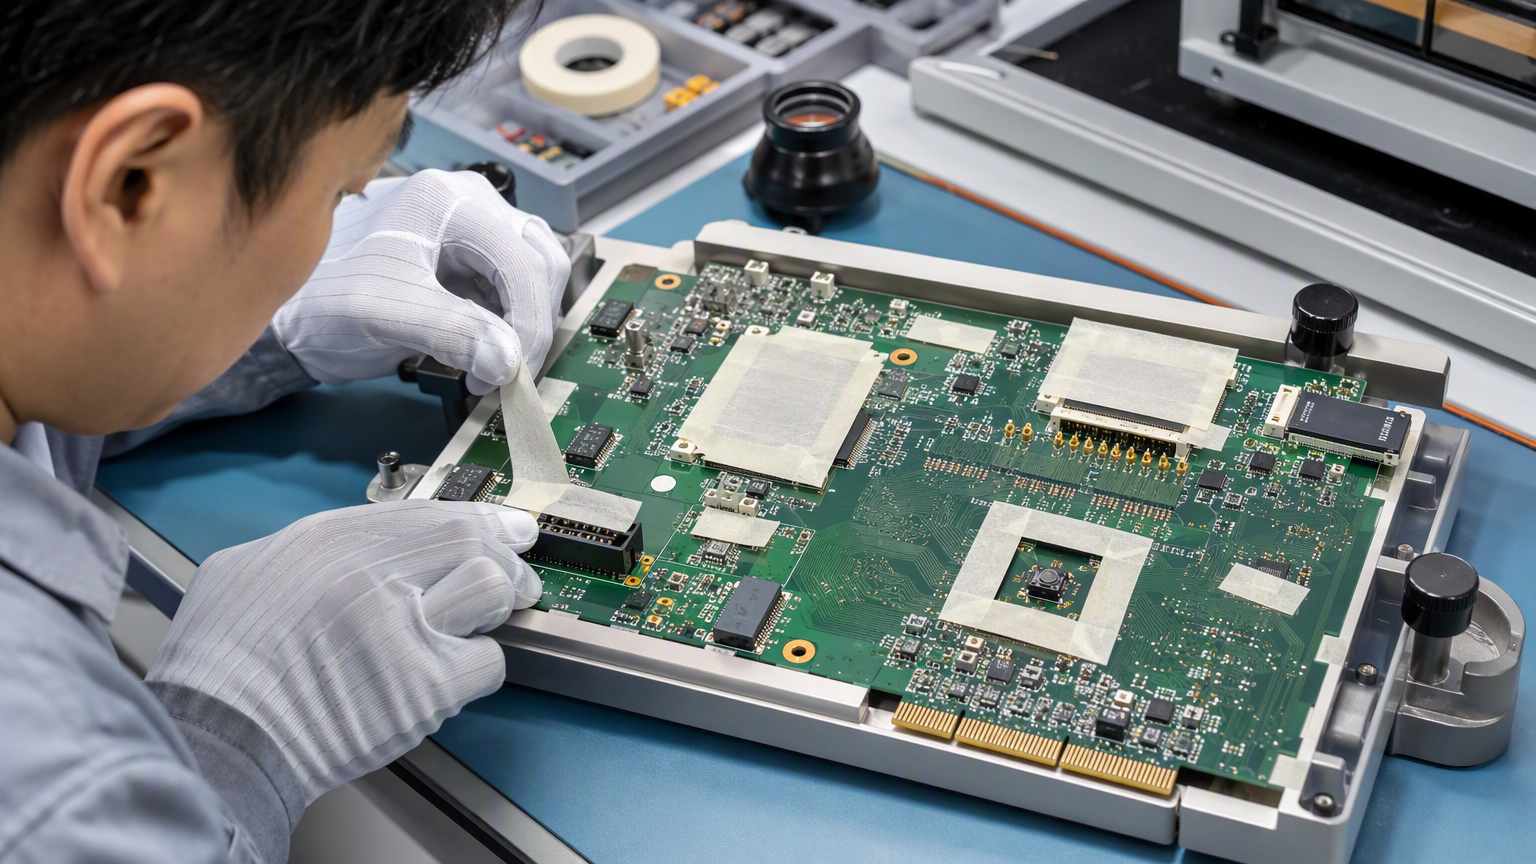
The process document should mark these areas in advance. The production team may use tape, peelable materials, or dedicated fixtures for masking. After the first article, the team should inspect the masking edge and demasking result. The coated board should also receive the required continuity and visual checks.
2.2 Sensors, Switches, Relays, and Moving Structures
Some sensors need exposure to air, pressure, light, or sound. Coating the active area may affect the sensor response. Switches and relays must also keep their normal movement. Material entering a contact or moving structure may affect switching and mechanical function.
The engineering team should therefore review the component structure. It can then define the keep-out boundary. First-article validation should include action, continuity, or response tests. A visual check alone cannot confirm normal function.
2.3 Heat-Dissipation Areas, Power Components, and Electrical Risk Zones
Power components and heat sinks need a suitable heat-transfer path. Coating a heat-dissipation surface may change the local thermal path. High-impedance, precision analog, and high-voltage areas also require separate evaluation.
The project can define the approach by reviewing electrical spacing, temperature rise, insulation condition, and customer requirements. Test conditions must match the product structure. Acceptable visual coverage cannot replace thermal and electrical function checks.
2.4 Document Coating Zones, Keep-Out Zones, and Inspection Points
Coating zones, keep-out zones, and inspection points should appear in the process documents. Assembly drawings, placement files, and customer-approved documents can support this definition. The BOM must match the actual components. Gerber files, BOM data, and production programs also require revision checks.
When the product data changes, the coating program should receive a synchronized review. Mixed revisions may cause wrong coating, missed coating, or test errors. NPI should include a cross-check of the complete data set.
3. Complete Engineering Documents and Surface Preparation Before Spraying
Preparation before spraying determines whether the next process remains under control. A clean surface, accurate boundary, and stable masking method create the basic conditions. A suitable material cannot compensate for poor preparation.
3.1 Use Gerber, BOM, Placement, and Assembly Data to Identify Risks
Gerber files can help identify traces, pads, and board areas. The BOM can help identify connectors, sensors, switches, and power components. Placement data can support spray-path planning. Assembly drawings can add component orientation and structural information.
These documents must remain consistent. The engineering team should also mark test points, gold fingers, heat-dissipation areas, high-voltage zones, and high-impedance zones. Documents support process decisions. They cannot replace engineering validation by themselves.
3.2 Confirm the Cleanliness of the PCB and Components
Dust, oil, and flux residue may affect coating adhesion. Residual moisture may also affect curing and insulation performance. The cleaning agent may create compatibility issues with the substrate, components, or coating.
The cleaning process should therefore follow the material documentation. After cleaning, the board needs drying and surface inspection. The production team should record abnormal boards, reworked boards, and cleaning status. Cleaning results should link to first-article and production records.
3.3 Establish the Masking and Demasking Method
The masking material must suit the coating and component surfaces. Masking must not damage solder joints or components. Demasking must not leave adhesive, fibers, or visible contamination.
The first-article stage should confirm the masking boundary. It should also check whether coating enters an interface area. Production should use a controlled masking method. Any method change requires a new sample validation.
4. Select the Coating Method for the Board and Production Model
Different coating methods suit different product structures. Manual spraying emphasizes operator consistency. Automated spraying emphasizes program and path control. Selective coating emphasizes coordinate, boundary, and keep-out management.
4.1 Manual Spraying for Samples and Low-Volume Validation
Manual spraying suits samples, low-volume builds, and process development. Operators need to control spray direction and coverage. They must also monitor atomization, path overlap, and overspray risk.
Spray distance, material viscosity, and operating parameters should follow the product TDS and equipment instructions. Process engineers should use samples to confirm coating continuity. One set of shop-floor parameters should not be copied to every product.
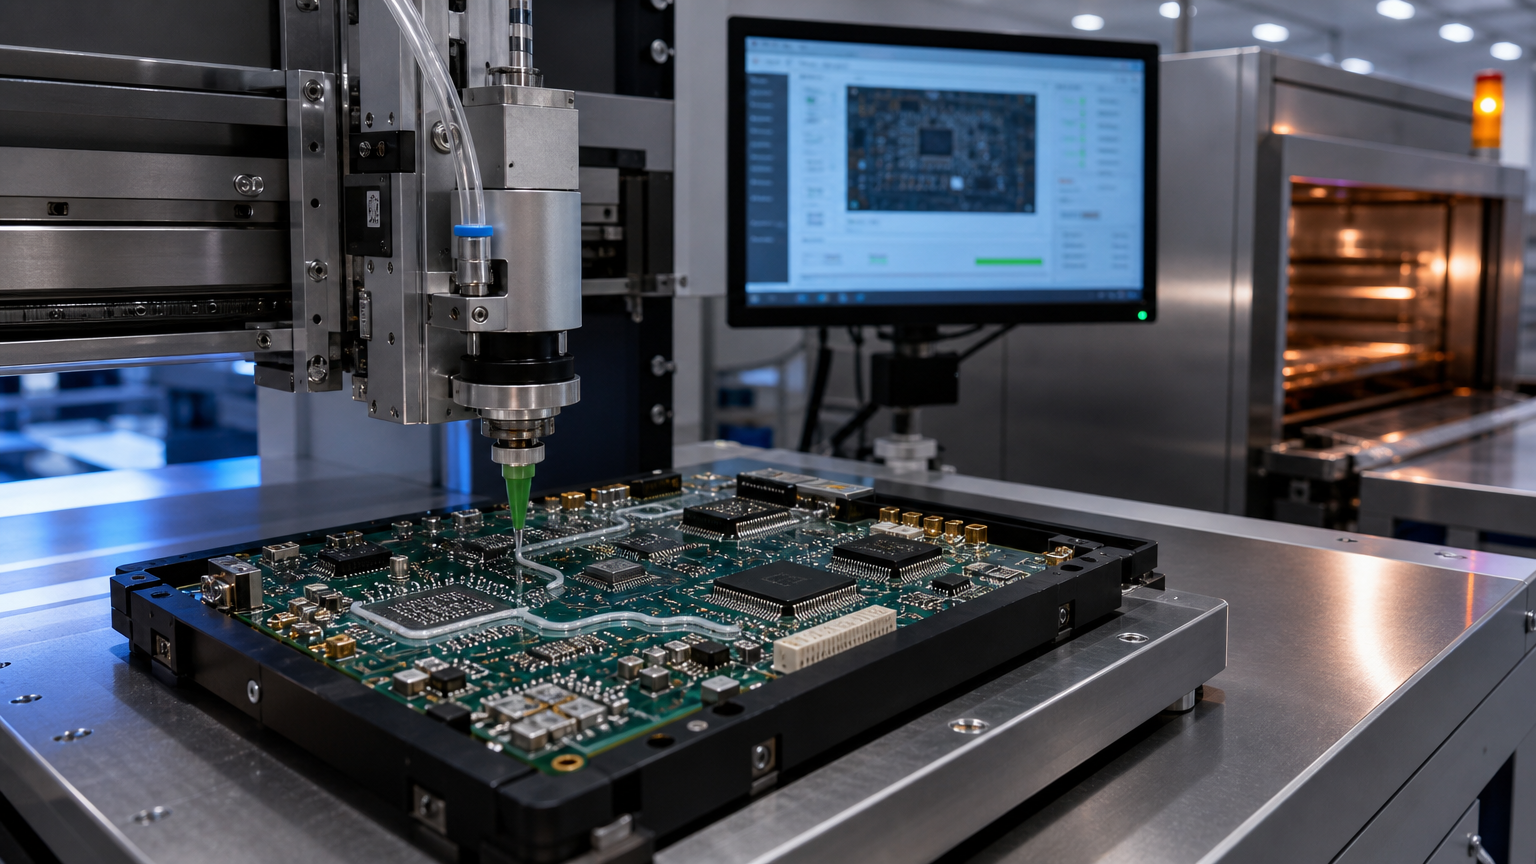
4.2 Automated and Selective Coating for Repeatable Production
Automated or selective coating can control the path through a programmed process. It suits projects with many sensitive components. The engineering team needs accurate coordinates and coating-zone data.
Automatic operation does not mean automatic acceptance. The first article still needs checks for missed coating, overspray, boundary position, bubbles, and component protection. Production also requires program revision and changeover control.
4.3 Brushing and Dipping as Conditional Alternatives
Brushing suits local touch-up, samples, and repair. It is flexible, but consistency depends on operators and process documents. Dipping can cover a larger surface area. It may suit products with few keep-out zones.
PCBA assemblies with complex connectors or dense sensors require careful dipping evaluation. Material entry into components, bubbles, and drainage also require inspection. The final method should follow the board structure and actual sample results.
5. The PCBA Conformal Coating Process on the Production Floor
The shop-floor process should form a continuous chain. Material control, cleaning, masking, coating, curing, demasking, and inspection all need records. PCBA conformal coating should not automatically use primer, intermediate, and topcoat layers. The product requirement should define the material system and layer structure.
5.1 Confirm Material Identity and Condition
Before production, verify the material model, batch, and expiration date. The team should also confirm storage condition and use requirements. Some materials require mixing or stirring. Others require specific application conditions.
The TDS and SDS provide important guidance. Materials should not be replaced without review. A material change requires new compatibility and process confirmation. The project should also retain material batch records.
5.2 Check Cleaning, Drying, and Line-Entry Conditions
Before line entry, inspect the board surface for cleanliness. Then confirm that the board is dry. Review the masking areas as well. Fixtures and tooling must remain clean.
The board should enter spraying only after the surface meets the required condition. Cleaning temperature, cleaning time, and drying method should follow the material documents and project specifications. Fixed values should not replace actual validation.
5.3 Control Spray Paths, Boundaries, and Film Thickness
During spraying, control the direction, path, and coverage boundary. Monitor atomization and coating continuity throughout the operation. The film should not show obvious missed areas, runs, or overspray.
Film thickness requirements should follow the material TDS and customer specifications. A measurement on a flat area cannot represent every component surface. Height changes, sharp edges, and complex structures may affect actual coverage. Inspection points should match product risk.
5.4 Confirm the Curing Method and Waiting Time
Different materials use different curing methods. Common paths include solvent evaporation, heat curing, moisture curing, UV curing, and combination curing. The project should select the method from the material documentation.
Curing equipment and shop-floor conditions also affect the result. After curing, confirm the surface condition and functional requirements. Do not claim that a board can be used immediately after spraying. Curing time should follow the TDS, equipment capability, and sample results.
5.5 Manage Demasking, Rework, and Local Touch-Up
Demasking requires the right timing. Demasking too early may damage the film. Demasking too late may increase removal difficulty. The timing should follow the material condition and process validation results.
Before rework, confirm the removal area. After local touch-up, inspect the boundary and curing condition again. Every rework operation should record the location, material batch, and action taken. These records support later traceability.
6. Verify the Coating with Visual, Coverage, Cure, and Functional Checks
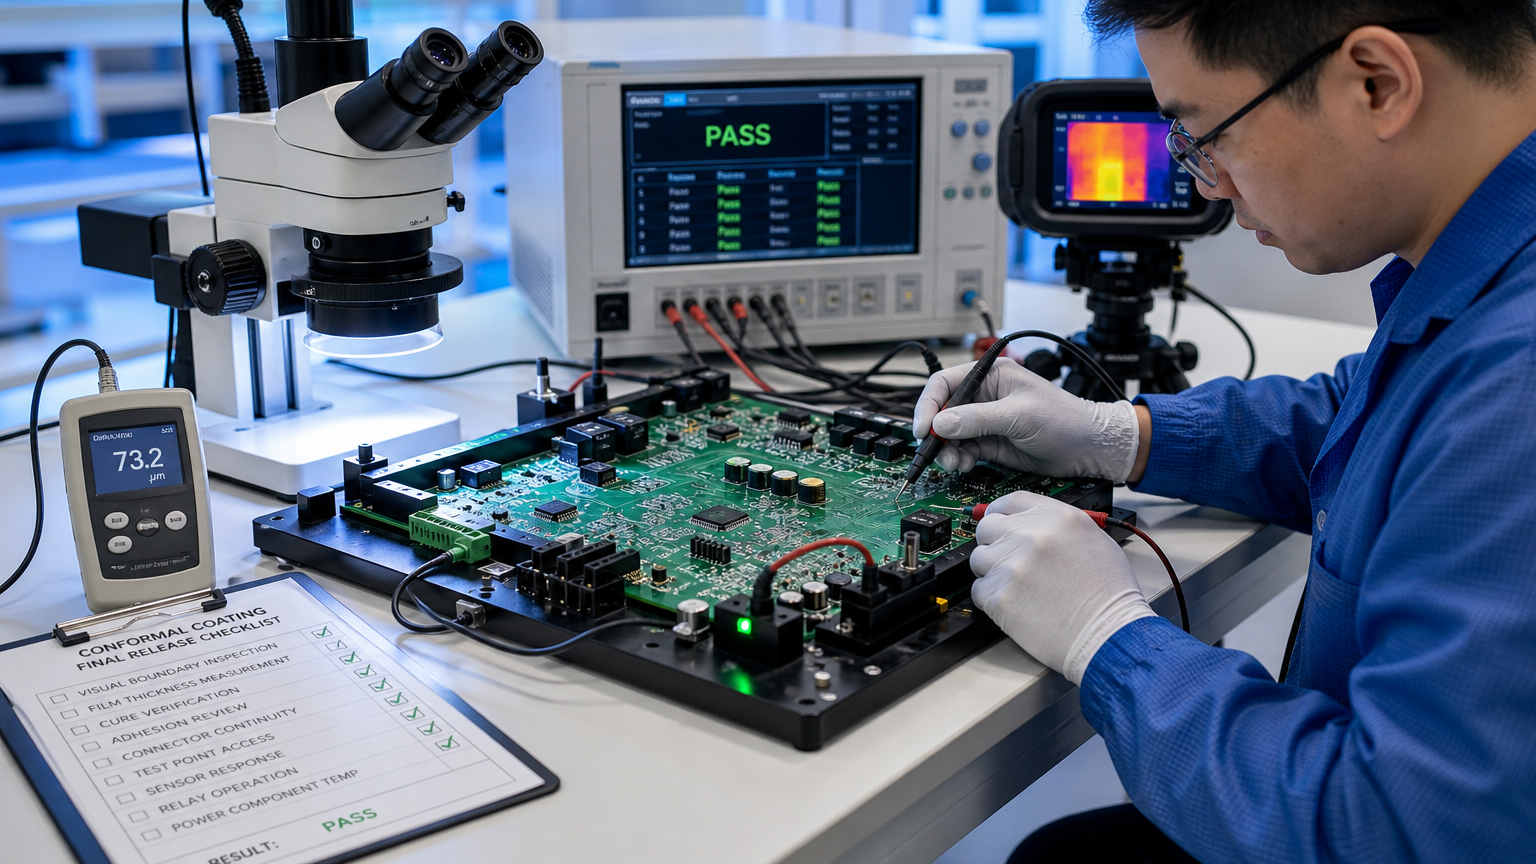
After coating, do not judge the result by surface color alone. Quality release should combine visual, boundary, coverage, cure, and functional checks. The inspection method should match the product risk and customer requirements.
6.1 Inspect Appearance and Coating Boundaries
Visual inspection should check missed coating, runs, bubbles, pinholes, and particles. Inspectors should also look for cracks, whitening, and boundary seepage. The masking area must remain clean.
Connectors, test points, component edges, and dense areas require special attention. Abnormal boards should be isolated. Inspection results must remain documented. Images or measurement data may be retained when needed.
6.2 Check Coverage and Film Thickness
The project should set inspection points for each coating zone. Material documents, customer specifications, and applicable standards should define film-thickness terms and measurement methods. Different surface shapes may produce different readings.
A single measurement point cannot represent the entire PCBA. High-risk areas need independent checks. The tool and sampling method should also match the material and substrate.
6.3 Confirm Cure, Adhesion, and Material Compatibility
The engineering team must confirm that the coating reaches the specified cure state. A tacky surface, whitening, or local softening requires review. Adhesion should also follow the project requirements.
In addition, inspect the solder mask, component housings, connector plastics, labels, and silkscreen. Cleaning agents and flux residue also require attention. Only a sample using the actual PCB and actual components can show board-level compatibility.
6.4 Complete Electrical and Functional Release Checks
Confirm connector continuity. Confirm test-point access. Confirm switch and relay operation. Confirm sensor response. Check power-component temperature rise under the relevant operating condition.
High-voltage and high-impedance areas also require applicable electrical tests. Visual acceptance cannot replace functional validation. Final release conditions should follow customer documents, applicable standards, and project specifications.
7. How to Evaluate a PCBA Supplier’s Conformal Coating Capability
Supplier evaluation should not rely on equipment photos alone. The engineering team should also review material control, zone documents, masking methods, and first-article validation. The production system should support program revision and material-batch traceability.
The supplier should explain how it handles connectors, sensors, test points, and heat-dissipation areas. It should also explain cleaning, spraying, curing, demasking, and rework. For selective coating projects, confirm the coordinate files, program revision, and boundary inspection method.
During quotation, provide Gerber files, a BOM, placement data, and assembly drawings. Include the operating environment and customer acceptance requirements. Choosing a PCBA supplier with real process assessment capability can reveal material compatibility, keep-out, and validation risks earlier.
7.1 Submit Gerber and BOM Data for a Conformal Coating Review
If the project includes connectors, sensors, switches, heat-dissipation components, or high-voltage areas, describe these requirements during quotation. The engineering team can then assess the coating zones, keep-out boundaries, coating method, material compatibility, and validation plan from the actual board data.
Submitting Gerber files, a BOM, placement data, and assembly drawings helps the supplier build a more accurate pcba manufacturing process assessment. Final material, film thickness, curing, testing, lead time, and quotation scope should follow the actual project data and confirmed results.
Conclusion
Conformal coating is not a single spraying action. It is a PCBA process chain that includes environmental assessment, zone definition, document preparation, surface treatment, spraying, curing, and quality verification. In pcba manufacturing projects, a suitable coating plan requires joint evaluation of materials, components, equipment, and acceptance requirements. Submit Gerber files and a BOM to begin a project-based discussion of conformal coating and pcba manufacturing needs.


Leave A Comment